
Short Engineering Answer
Heat set inserts fail in Voron 3D printer assemblies when the printed fastening structure cannot maintain preload, boss support, torque resistance, or insert retention under heat, vibration, repeated maintenance, and frame-mounted loads.
Voron-style 3D printer parts often combine heat exposure, motor vibration, belt tension, repeated service access, compact printed bosses, and long-term screw preload. These conditions can make heat set insert joints loosen, spin, pull out, crack the boss, or lose clamping force over time.
The insert itself is usually not the weakest point. Most failures come from the surrounding printed boss, material behavior, installation quality, screw engagement length, hole size, and load direction.
A heat set insert can work well in Voron assemblies, but the printed part must be designed for printer heat, vibration, maintenance, and mechanical load, not only for insert installation.
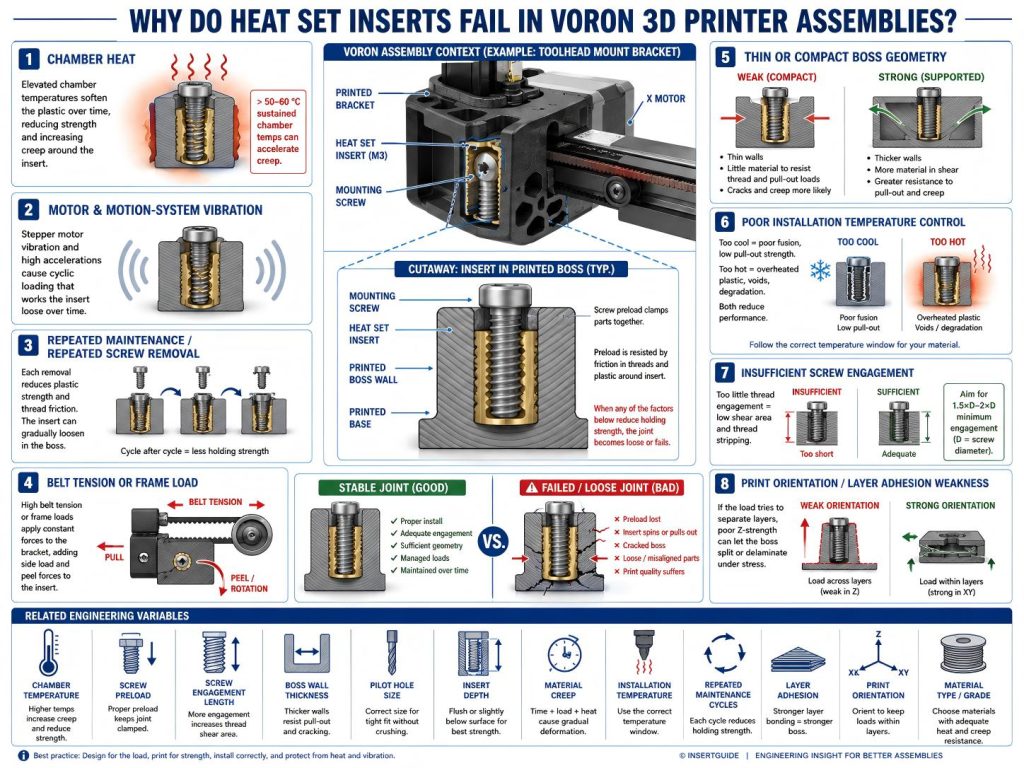
Root Causes
Heat From Enclosed Printer Chambers
Voron printers are often enclosed and may operate at elevated chamber temperatures.
Heat can reduce the stiffness of printed materials and increase creep under screw preload. PETG, ABS, ASA, and other materials respond differently, but any printed boss can lose stability if the temperature, preload, and geometry exceed its design margin.
The part does not need to melt for insert reliability to drop. Moderate heat can still increase preload relaxation, boss deformation, and long-term joint movement.
Repeated Printer Maintenance
Voron assemblies are often serviced, tuned, upgraded, or repaired.
Panels, toolhead parts, electronics mounts, belt path components, skirts, hinges, covers, and brackets may be opened or adjusted repeatedly. Each screw removal and reinstallation transfers torque into the insert and surrounding printed boss.
Over time, repeated assembly can reduce preload stability, wear the plastic-to-insert interface, or make the insert more likely to spin during tightening.
Motor and Motion System Vibration
Voron printers contain motors, belts, moving gantries, fans, and toolhead motion.
These systems create vibration and cyclic loading. If the insert joint has weak preload, short screw engagement, poor boss support, or creep-sensitive material behavior, vibration can gradually reduce stability.
The result may appear as loose screws, insert movement, rattling panels, or reduced alignment stability.
Belt Tension and Frame Loads
Some Voron printed parts carry belt tension, frame alignment load, or mechanical support load.
If a heat set insert is placed in a part that receives belt tension, bracket load, or alignment force, the insert joint may experience more than simple screw clamping.
A weak boss may deform, crack, or lose preload under sustained load. If the load path is not supported by enough surrounding plastic, the insert may loosen or pull out.
Thin or Compact Boss Geometry
Voron printed parts are often compact and optimized for fit inside printer assemblies.
Compact geometry can leave limited boss wall thickness, shallow insert depth, or bosses close to edges and cutouts. These features reduce support around the insert.
A correct hole size is important, but it cannot compensate for a boss that lacks enough material to resist screw preload, vibration, and service cycles.
Poor Installation Temperature Control
Heat set insert installation must create controlled plastic flow around the insert.
If the insert is installed too cold, the plastic may not flow fully around the knurling. If it is installed too hot, the boss may over-soften, collapse, or lose dimensional accuracy.
For Voron parts, installation damage may not appear immediately. It can show up later as loosening after heat, vibration, or repeated maintenance.
Insufficient Screw Engagement
Short screw engagement can reduce long-term reliability.
If the screw engages too few threads, load is concentrated over a shorter length of the insert. This can reduce preload stability and make the joint more sensitive to vibration, repeated assembly, or thermal cycling.
Enough screw engagement helps distribute load through the insert and printed boss.
Print Orientation and Layer Adhesion
FDM printed Voron parts are directionally strong.
If screw load, belt tension, or bracket load acts across weak layer lines, the part may crack or delaminate near the insert. This can reduce pull-out strength and boss stability even if the insert itself is properly installed.
Print orientation should be selected with the real load direction in mind, especially for brackets, mounts, hinges, and toolhead-related parts.
Related Engineering Variables
Heat set insert reliability in Voron 3D printer assemblies depends on several connected variables:
- Chamber temperature
- Motor vibration
- Belt tension
- Screw preload
- Tightening torque
- Screw engagement length
- Boss wall thickness
- Boss height
- Pilot hole size
- Insert depth
- Material creep
- Installation temperature
- Repeated maintenance cycles
- Layer adhesion
- Print orientation
- Frame load
- Toolhead or gantry motion
These variables should be evaluated together. A heat set insert joint may work well in a lightly loaded cover but fail in a bracket, hinge, belt-related mount, or repeatedly serviced printer component.
Voron insert reliability is not only about thread durability. It is about maintaining preload, boss support, and load-path stability under real printer conditions.
Engineering Interpretation
Heat set insert failure in Voron assemblies is usually a heat, vibration, and serviceability problem.
The failure may appear as:
- Insert loosening from preload loss
- Insert spin during repeated maintenance
- Pull-out from belt or bracket load
- Boss deformation from chamber heat and screw preload
- Boss cracking from compact geometry or over-tightening
- Layer separation from poor print orientation
- Rattling covers or unstable mounted components
These failures often overlap.
For example, a compact boss may install cleanly at first. After chamber heat, repeated servicing, and printer vibration, the boss may creep or lose preload. The insert may then begin to loosen or spin during later screw removal.
This is why Voron insert joints should be designed for long-term printer use, not only for a clean first assembly.
How to Reduce the Risk
To reduce heat set insert failure in Voron 3D printer assemblies:
- Use enough boss wall thickness around each insert.
- Avoid thin, unsupported, or edge-adjacent bosses.
- Use the correct pilot hole size for the printed material.
- Control insert installation temperature carefully.
- Avoid overheating the boss during insertion.
- Use enough screw engagement length.
- Avoid excessive screw torque.
- Choose material based on chamber heat, creep, and load.
- Improve print orientation around loaded insert joints.
- Support high-load bosses with surrounding geometry or ribs.
- Design serviceable parts for repeated screw removal.
- Consider vibration from motors, fans, belts, and gantry motion.
- Avoid relying on high preload in small printed bosses.
A reliable Voron insert joint is a supported fastening structure. The insert provides durable threads, but the printed boss must maintain shape, preload, and load support through heat, motion, and maintenance.
Related InsertGuide Pages
- Why Do Heat Set Inserts Fail Under Vibration?
- Why Does Screw Preload Drop in 3D Printed Insert Joints?
- Why Does Repeated Assembly Weaken Heat Set Inserts?
- Why Do Threaded Inserts Loosen After Repeated Screw Removal?
- What Causes Boss Deformation Around Heat Set Inserts?
- Heat Set Insert Installation Temperature for 3D Printed Parts
- Screw Engagement Length for Heat Set Inserts in 3D Printed Parts
- How to Design Bosses for Heat Set Inserts
- Layer Adhesion and Heat Set Insert Strength in 3D Printed Parts
FAQ
Are heat set inserts reliable in Voron 3D printer parts?
Yes. Heat set inserts can be reliable in Voron parts when the boss, hole size, installation temperature, material, screw engagement, and load path are designed correctly. Problems usually appear when heat, vibration, or repeated service weakens the printed structure around the insert.
Why do inserts loosen in Voron printed parts?
Inserts loosen in Voron parts when chamber heat, vibration, repeated maintenance, material creep, weak boss geometry, or poor screw engagement reduces preload and plastic-to-insert stability.
Can enclosed printer heat weaken heat set insert joints?
Yes. Enclosed printer heat can reduce plastic stiffness and increase creep under screw preload. This can cause preload loss, boss deformation, or insert loosening over time, especially in compact or thin bosses.