
PLA vs PETG fastening behavior for heat set inserts affects pull-out strength, boss stability, repeated assembly durability, and long-term fastening reliability in 3D printed parts.
Successful insert performance depends on more than insert geometry alone.
Material behavior strongly affects:
- pull-out resistance
- boss stability
- torque behavior
- repeated assembly durability
- layer adhesion
- creep deformation
- long-term fastening reliability
Understanding the differences between PLA and PETG helps engineers design fastening systems that match real operational conditions.
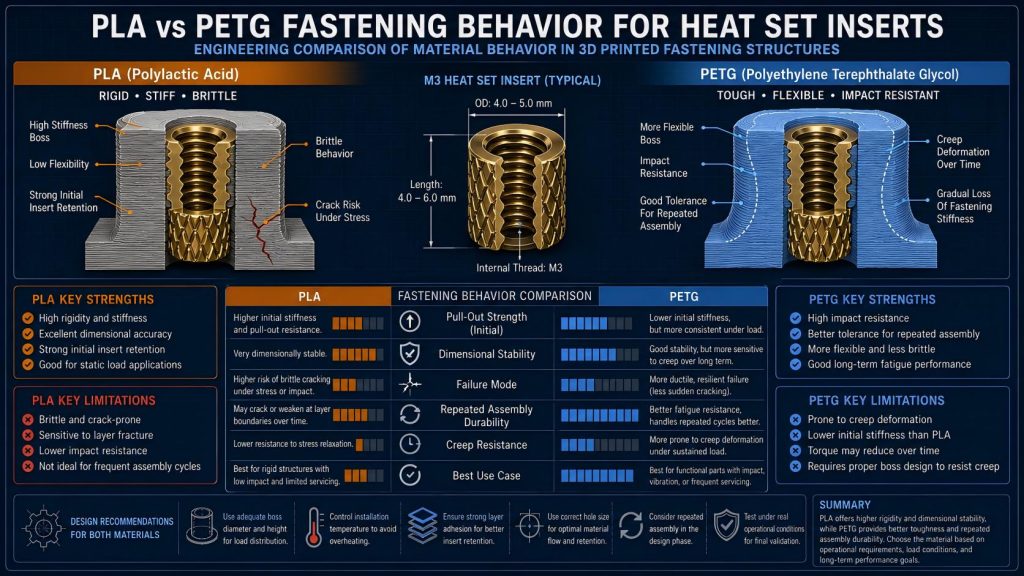
PLA Fastening Behavior
PLA is commonly used because it is:
- easy to print
- dimensionally stable
- relatively stiff
- capable of producing clean insert installations
The higher stiffness of PLA often provides:
- strong initial insert retention
- stable boss geometry
- good dimensional consistency
However, PLA also has limitations.
Under repeated loading or impact conditions, PLA may become:
- brittle
- crack-prone
- sensitive to cyclic stress
Repeated assembly may gradually weaken surrounding boss structures, especially in thin unsupported geometries.
PLA stiffness can improve short-term rigidity, but localized stress concentration around the insert cavity may increase the risk of boss cracking under repeated tightening or installation stress. For more detail, see our troubleshooting guide on why bosses crack around heat set inserts.
PETG Fastening Behavior
PETG behaves differently under fastening loads.
Compared with PLA, PETG is generally:
- more flexible
- more impact resistant
- less brittle
- more tolerant of repeated loading
This flexibility may improve long-term durability in assemblies exposed to:
- vibration
- repeated assembly
- impact loading
- service access cycles
However, PETG may also experience:
- creep deformation
- gradual boss expansion
- reduced torque consistency over time
Fastening structures designed for PETG often require more attention to boss geometry and long-term load distribution.
PETG creep and long-term deformation can gradually reduce screw preload and fastening stability during repeated assembly cycles. When this happens, the insert may remain seated while the joint itself becomes less reliable. For a related failure pattern, see our guide on why threads become loose in heat set inserts.
PLA vs PETG Fastening Behavior for Heat Set Inserts
PLA vs PETG fastening behavior for heat set inserts differs significantly in rigidity, creep resistance, repeated assembly performance, and long-term fastening stability.
Pull-Out Strength Differences
PLA often provides higher short-term pull-out stiffness because of its rigidity.
PETG may provide lower initial stiffness but improved long-term durability under cyclic loading.
In repeated assembly structures, pull-out stability depends heavily on:
- boss support
- insert geometry
- layer adhesion
- operational load conditions
Related Guide:
M3 Heat Set Insert Pull-Out Strength for 3D Printed Parts
Boss Design Considerations
Boss geometry behaves differently between PLA and PETG.
PLA bosses often maintain dimensional rigidity but may crack under excessive installation stress.
PETG bosses may better absorb stress but can gradually deform under sustained tightening loads.
Both materials benefit from:
- balanced wall thickness
- stable load distribution
- proper installation temperature
- sufficient boss support
Related Guide:
M3 Heat Set Insert Boss Design for 3D Printed Parts
Repeated Assembly Performance
Repeated assembly highlights major differences between PLA and PETG.
PLA may gradually weaken through cyclic cracking near layer boundaries.
PETG often tolerates repeated loading more effectively but may slowly lose fastening stiffness over time.
For serviceable assemblies requiring long-term maintenance access, PETG is often preferred because of its improved fatigue tolerance.
Related Guide:
Recommended Fastening Structure for Repeated Assembly PETG Parts
Layer Adhesion Behavior
Layer adhesion strongly affects fastening reliability in both materials.
Weak layer bonding may reduce:
- pull-out strength
- torque stability
- boss durability
PETG generally provides improved interlayer bonding compared with PLA but may also become more sensitive to deformation during thermal insert installation.
Common Failure Differences
PLA
Typical failure modes include:
- brittle cracking
- layer fracture
- boss splitting
- sudden failure under impact loading
In repeated assembly, these PETG failure modes often come from creep, preload loss, and gradual torque instability rather than a single installation error.
PETG
Typical failure modes include:
- creep deformation
- gradual loosening
- boss expansion
- reduced torque consistency
Material Behavior Is Part of the Fastening System
Insert selection alone cannot determine fastening reliability.
Successful fastening performance depends on the interaction between:
- material behavior
- insert geometry
- boss structure
- pull-out resistance
- installation conditions
- repeated assembly requirements
PLA and PETG require different fastening strategies based on operational loading conditions and long-term service requirements.
Conclusion
PLA and PETG provide very different fastening behavior for heat set inserts used in 3D printed parts.
PLA offers higher rigidity and dimensional stability, while PETG often provides improved flexibility and fatigue resistance under repeated loading conditions.
Reliable fastening systems should always be designed around material behavior rather than insert geometry alone.
Related Engineering Guides
- How to Choose Heat Set Inserts for 3D Printed Parts
- Heat Set Insert Hole Size Guide
- How to Design Bosses for Heat Set Inserts
- PLA vs PETG vs ABS for Threaded Inserts
- Why Heat Set Inserts Fail in 3D Printed Parts
- Pull-Out Strength of Heat Set Inserts in 3D Printed Parts
- Torque Resistance of Heat Set Inserts in 3D Printed Parts
- Layer Adhesion and Heat Set Insert Strength in 3D Printed Parts
- Heat Set Insert Installation Temperature for 3D Printed Parts
- Screw Engagement Length for Heat Set Inserts in 3D Printed Parts
Related Decision Resources
For insert selection, tool choice, and supplier comparison, use these decision-focused references after the engineering requirements are defined.