
Heat set inserts in CNC fixture plates are used to create durable threaded points for clamps, locating stops, sacrificial plates, guide blocks, and modular workholding components. In 3D printed CNC fixture plates, these inserts help printed plastic parts survive repeated tightening, setup changes, and light workholding loads.
Heat set inserts help 3D printed CNC fixture plates become more practical because they create durable metal threads for clamps, stops, guide blocks, sacrificial plates, and removable fixture elements.
But CNC fixture plates are not ordinary printed panels.
They may experience screw torque, clamping force, vibration, repeated repositioning, and contact with cutting tools, chips, coolant, dust, or workpiece debris. For this reason, insert design must be treated as part of the fixture plate’s mechanical structure.
The key point is:
A 3D printed CNC fixture plate should use heat set inserts as reinforced workholding points, not just convenient threaded holes.
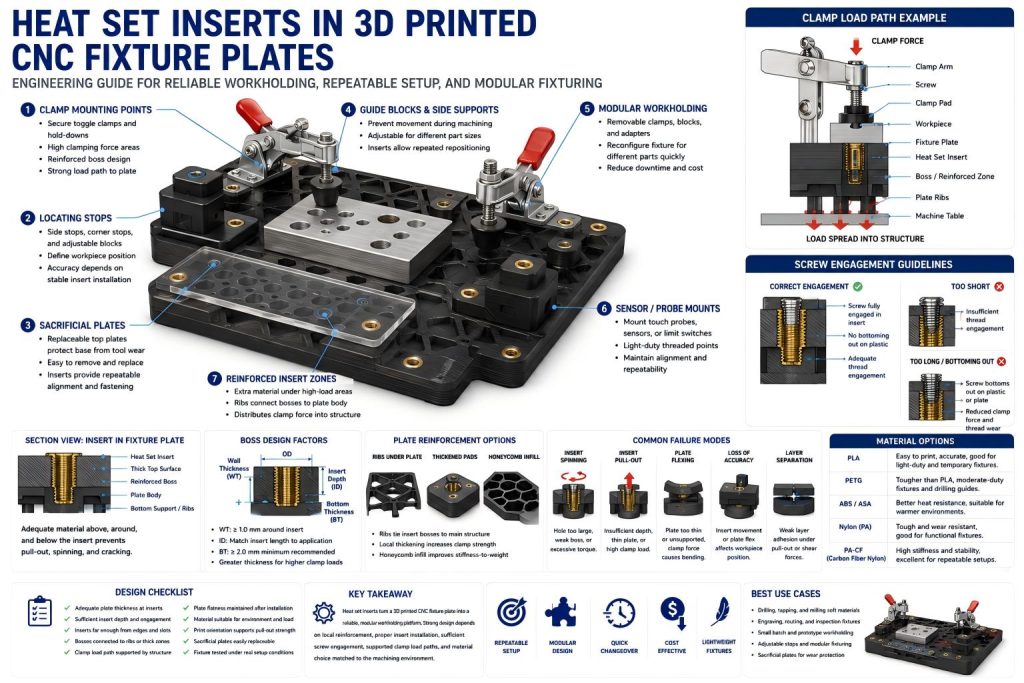
Why 3D Printed CNC Fixture Plates Use Heat Set Inserts
A CNC fixture plate often needs multiple threaded points. These points may hold clamps, locating stops, removable blocks, side supports, reference edges, or replaceable wear surfaces.
Printed plastic holes can work for a simple prototype, but they are not ideal for repeated clamping. Threads printed directly into plastic can wear out, deform, strip, or lose consistency when screws are tightened repeatedly.
Heat set inserts are useful because they provide:
- reusable metal threads
- better screw retention
- more durable clamp mounting points
- easier replacement of stops and blocks
- better repeatability during setup
- improved serviceability
- reduced thread wear in printed plates
- modular fixture reconfiguration
In CNC fixture plates, the insert is not only holding a screw. It is helping the fixture maintain position and clamping behavior over repeated use.
A weak insert location may not fail immediately, but it can slowly reduce fixture accuracy.
Common Insert Locations in CNC Fixture Plates
Heat set inserts are usually placed in areas where fixture hardware needs to be tightened, removed, adjusted, or replaced.
Clamp Mounting Points
Clamp mounting points are often the most demanding insert locations. A clamp screw applies force to hold the workpiece in place. For clamp screws that are tightened repeatedly, torque resistance helps prevent inserts from rotating inside the printed plate or reinforced boss. That force travels through the clamp, screw, insert, boss, and fixture plate body.
If the insert area is weak, the clamp may loosen, tilt, pull the insert upward, or deform the fixture plate.
Clamp insert locations should have enough surrounding material and should be tied into thicker plate regions, ribs, or reinforced zones when possible.
Locating Stops
Locating stops define where a workpiece sits on the fixture plate. These may be side stops, corner stops, dowel-like features, or removable printed blocks.
The insert load may not be as high as a clamp load, but accuracy matters more. If the insert shifts or the stop no longer sits flat, the workpiece location may change.
For locating stops, insert installation must avoid distorting the reference surface.
Replaceable Sacrificial Plates
Some CNC fixture plates use sacrificial top plates or replaceable pads. These are useful when drilling, engraving, cutting, or routing may damage the contact surface.
Heat set inserts allow sacrificial plates to be replaced without rebuilding the entire fixture.
The insert pattern should be placed so that replacement plates can be aligned repeatably and tightened without bending the printed base.
Guide Blocks and Side Supports
Guide blocks help position the workpiece or prevent side movement during cutting or drilling. These blocks may be adjusted for different part sizes.
Heat set inserts make guide blocks more modular because they allow repeated repositioning without damaging printed threads.
Vacuum, Sensor, or Probe Mounts
Some printed CNC fixture plates include vacuum channels, probe mounts, limit switch brackets, or sensor holders. These inserts may carry lighter loads, but alignment and sealing can matter.
In these areas, insert installation should not distort flat surfaces, channels, or reference geometry.
Clamping Force and Fixture Plate Load Paths
A common mistake in printed CNC fixture design is treating the fixture plate as a flat object with threaded holes.
In real use, each clamped screw creates a load path.
The screw force moves from the screw head into the clamp, from the clamp into the workpiece or fixture element, from the screw into the insert, from the insert into the boss or plate, and from the plate into the larger support surface.
If the insert is unsupported, the local area may flex or deform. If the fixture plate is too thin, tightening the clamp can bend the plate instead of holding the workpiece securely.
For clamp locations, pull-out strength should be evaluated together with local plate thickness and support under the clamping load.
A good CNC fixture plate insert design should consider:
- the direction of clamp force
- whether the insert is loaded in tension or shear
- whether the plate bends under tightening
- whether the insert is close to an edge
- whether the clamp is supported by nearby material
- whether the boss is connected to ribs or thicker plate sections
- whether repeated tightening will loosen the insert over time
A fixture plate does not need to be heavy everywhere. But it does need strength where screws transfer force.
Boss Design for CNC Fixture Plate Inserts
Many fixture plates are designed as relatively flat panels. This can create a challenge because heat set inserts need enough material around and below them. For printed fixture plates, boss design should focus on local reinforcement around clamp and stop locations rather than making the entire plate unnecessarily bulky.
If the plate is too thin, the insert may not have enough depth for retention. If the insert is too close to the surface, screw engagement may be limited. If the insert is too close to the edge, the surrounding plastic may crack or pull out.
Important boss and plate design factors include:
- local plate thickness around the insert
- insert depth
- bottom material thickness
- wall thickness around the insert hole
- distance from edges
- spacing between inserts
- support ribs under the plate
- counterbore or relief for mating hardware
- clearance for clamp movement
- screw length and engagement
For thin fixture plates, local thickening may be needed around inserts. This can be done with raised bosses, underside ribs, thickened pads, or reinforced zones under clamp locations.
The goal is to make each insert location strong enough without making the entire fixture plate unnecessarily bulky.
Insert Depth and Screw Engagement
Screw engagement is especially important in CNC fixture plates because clamps and stops may be tightened repeatedly.
If screw engagement is too short, the screw may loosen or fail to create consistent clamping force. If the screw is too long, it may bottom out inside the insert or press into the plastic below the insert.
For fixture plate applications, screw engagement should be matched to:
- insert length
- screw diameter
- clamp height
- expected tightening torque
- number of setup cycles
- plate thickness
- fixture hardware stack height
- material strength
The screw should fully engage the insert without using the plastic beneath the insert as a hard stop.
A screw that bottoms out can feel tight while providing poor clamping force. That is a small mechanical lie, and CNC fixtures dislike lies.
Material Choice for 3D Printed CNC Fixture Plates
Material choice depends heavily on the machining environment and load level.
PLA
PLA can be useful for light-duty fixture plates, engraving fixtures, inspection plates, drilling templates, and temporary setups. It prints accurately and stays dimensionally stable in normal room-temperature conditions.
However, PLA is brittle and heat sensitive. It is not ideal for warm environments, high clamping force, coolant exposure, impact, or aggressive machining vibration.
PLA fixture plates should use conservative insert design and generous support around clamp points.
PETG
PETG provides better toughness than PLA and can work for moderate-duty fixture plates. It is less brittle, but it can flex under clamping load.
PETG fixture plates should be designed with enough thickness and rib support to prevent bending or creep around insert locations.
ABS and ASA
ABS and ASA provide better heat resistance and can be useful for fixtures exposed to warmer environments or repeated handling. They may be suitable for more functional fixture plates if printed accurately.
Layer adhesion and warping must be controlled because fixture plates depend on flatness and repeatability.
Nylon and Carbon Fiber Nylon
Nylon and carbon fiber nylon are strong options for functional fixture plates, especially when toughness, wear resistance, and stiffness matter.
Carbon fiber nylon can improve stiffness and reduce plate flex, which helps with repeatability. However, insert installation must be controlled carefully, and reinforced boss geometry is still needed.
A stronger material helps, but the insert still needs support from the surrounding structure.
Flatness, Accuracy, and Insert Installation
CNC fixture plates depend on accuracy. Even if the insert does not fail mechanically, poor installation can reduce fixture performance.
Problems may include:
- tilted inserts
- raised plastic around the insert
- warped local surfaces
- insert sitting above the plate surface
- softened material near reference features(For accuracy-critical fixture plates, installation temperature should be controlled so the insert seats cleanly without raising material or distorting reference surfaces.)
- misaligned clamp or stop holes
- distorted sacrificial plate mounting points
For clamp locations, minor surface distortion may be acceptable if it does not affect workholding. For locating stops, guide blocks, probe mounts, or reference edges, distortion can directly affect accuracy.
To improve installation quality:
- use the correct hole size
- insert straight and perpendicular to the plate
- avoid excessive heat
- avoid excessive pressure
- allow the insert to cool before loading it
- test installation on sample geometry
- keep reference surfaces away from excessive heat zones
- clean raised material if it affects mating hardware
A fixture plate is only repeatable if its reference features remain stable.
Replaceable Plates and Modular Workholding
One of the strongest reasons to use heat set inserts in printed CNC fixture plates is modularity.
A printed fixture plate can support removable parts such as:
- sacrificial plates
- clamp blocks
- stop blocks
- side guides
- drill bushings
- engraving supports
- sensor brackets
- vacuum channel covers
- product-specific adapters
This allows the base fixture to remain in use while smaller components are replaced or reconfigured.
For small production runs, this is valuable because part geometry may change often. Instead of redesigning the entire fixture, only the replaceable block or plate needs to be updated.
Heat set inserts turn the printed plate into a reusable platform rather than a disposable part.
CNC-Specific Limitations of Printed Fixture Plates
3D printed CNC fixture plates are useful, but they have limits.
They are generally better suited for:
- light machining
- drilling guides
- engraving
- routing soft materials
- inspection fixtures
- assembly support
- small batch positioning
- low-force workholding
- soft jaws or support blocks
- prototype machining setups
They are not always appropriate for high-force machining, heavy metal cutting, high-temperature operations, aggressive coolant environments, or situations where fixture stiffness must match metal tooling.
Important limitations include:
- lower stiffness than metal plates
- possible creep under sustained clamp load
- reduced heat resistance
- lower thread strength if inserts are poorly supported
- risk of layer separation
- potential loss of flatness
- sensitivity to print orientation
- lower wear resistance in contact zones
The best use of printed CNC fixture plates is not to imitate metal tooling blindly. It is to use printed structures where customization, speed, and modularity matter, while respecting the mechanical limits of plastic.
Common Failure Modes in CNC Fixture Plate Inserts
Heat set inserts in printed CNC fixture plates fail in several common ways.
Insert Spinning
The insert rotates inside the plastic during screw tightening or removal.
Common causes include:
- oversized hole
- overheated installation
- weak boss wall
- excessive screw torque
- repeated clamp adjustment
- insufficient material around the insert
Insert spinning is especially common when clamps are tightened aggressively.
Insert Pull-Out
The insert pulls upward out of the fixture plate under clamp force or repeated tension.
Causes may include:
- shallow insert depth
- thin plate section
- weak bottom support
- poor layer orientation
- high clamp load
- insert too close to an edge
- boss not reinforced
Clamp mounting points and replaceable plate screws are common pull-out locations.
Plate Flexing
The insert may stay in place while the plate itself bends. This can reduce clamping reliability and part accuracy.
Plate flexing can occur when:
- the fixture base is too thin
- ribs are missing
- clamps are placed far from support
- the workpiece is unevenly supported
- the printed material is too flexible
- the insert load is concentrated in one area
Loss of Positioning Accuracy
A fixture plate may lose accuracy if stop blocks, guide blocks, or reference features shift over repeated use.
This can happen because of:
- insert movement
- plastic creep
- screw loosening
- surface distortion during installation
- clamp force bending the plate
- wear around removable blocks
In CNC fixture plates, accuracy loss can be more important than visible failure.
Layer Separation
Layer separation may occur when pull-out or clamp forces act across weak printed layers.
This is especially risky around inserts placed in thin walls, tall bosses, or unsupported edge locations.
Design Checklist for CNC Fixture Plate Inserts
Before using heat set inserts in a 3D printed CNC fixture plate, check the following:
- Is the insert used for clamping, locating, replacement, or light mounting?
- Does the insert location have enough local plate thickness?
- Is there enough material below the insert?
- Is the insert far enough from edges and slots?
- Is the screw engagement length sufficient?
- Will the screw be tightened repeatedly?
- Is the clamp force supported by the plate structure?
- Does the plate need ribs or local thickening?
- Will the fixture plate bend under load?
- Are locating stops protected from installation distortion?
- Can sacrificial plates be replaced without damaging the base?
- Is the material suitable for machining environment and clamp force?
- Does print orientation support pull-out and torque loads?
- Could chips, heat, coolant, or dust affect the fixture?
- Has the fixture been tested under real setup conditions?
A CNC fixture plate should be evaluated as a working tool, not only as a printed part.
Engineering Takeaway
Heat set inserts can make 3D printed CNC fixture plates more durable, modular, and practical for small batch workholding, inspection, engraving, drilling, routing, and light machining setups.
They are especially useful for:
- clamp mounting points
- locating stops
- replaceable sacrificial plates
- guide blocks
- modular workholding elements
- sensor or probe mounts
- product-specific adapters
But the insert is only one part of the fixture system.
Reliable performance depends on:
- correct hole size
- controlled insert installation
- enough local plate thickness
- reinforced boss geometry
- sufficient screw engagement
- supported clamp load paths
- suitable material choice
- stable print orientation
- preserved fixture flatness and accuracy
A printed CNC fixture plate should not simply copy a metal plate with holes.
It should use 3D printing where it is strongest: customized geometry, modular replaceable features, fast iteration, and local reinforcement around the areas that actually carry load.
Related Failure Question
CNC fixture plates expose insert joints to clamping force, repeated setup cycles, locating loads, pull-out stress, and torque demand. For failure diagnosis, see why heat set inserts fail in 3D printed fixtures.
FAQ
Can heat set inserts be used in 3D printed CNC fixture plates?
Yes. Heat set inserts can be used in 3D printed CNC fixture plates for clamps, locating stops, sacrificial plates, guide blocks, and modular fixture components. They provide reusable metal threads and improve serviceability compared with printed plastic threads.
Are 3D printed CNC fixture plates strong enough for machining?
They can be useful for light machining, drilling guides, engraving, inspection, routing soft materials, and small batch positioning. They are not always suitable for high-force metal cutting or applications that require metal-level stiffness.
Where should inserts be placed in a printed CNC fixture plate?
Inserts should be placed where clamps, stops, replaceable plates, guide blocks, or modular components need durable threaded connections. Insert locations should have enough local thickness, support, and distance from edges.
What causes inserts to fail in CNC fixture plates?
Common causes include thin plate sections, insufficient insert depth, poor installation temperature, excessive clamp torque, weak layer orientation, unsupported bosses, and plate flexing under clamping load.
What material is best for 3D printed CNC fixture plates with inserts?
PLA can work for light-duty and accurate temporary fixtures. PETG is tougher but more flexible. ABS and ASA offer better heat resistance. Nylon and carbon fiber nylon are better for stronger functional fixture plates, but boss design and print orientation remain critical.
Related Engineering Guides
- How to Choose Heat Set Inserts for 3D Printed Parts
- Heat Set Insert Hole Size Guide
- How to Design Bosses for Heat Set Inserts
- PLA vs PETG vs ABS for Threaded Inserts
- Why Heat Set Inserts Fail in 3D Printed Parts
- Pull-Out Strength of Heat Set Inserts in 3D Printed Parts
- Torque Resistance of Heat Set Inserts in 3D Printed Parts
- Layer Adhesion and Heat Set Insert Strength in 3D Printed Parts
- Heat Set Insert Installation Temperature for 3D Printed Parts
- Screw Engagement Length for Heat Set Inserts in 3D Printed Parts
Related Decision Resources
For insert selection, tool choice, and supplier comparison, use these decision-focused references after the engineering requirements are defined.