
M3 heat set insert installation depends on more than simply heating a brass insert and pressing it into a printed hole. Reliable installation requires the right pilot hole, controlled heat, straight insertion, enough hole depth, proper seating depth, and enough surrounding boss material to support the insert after it cools.
M3 is one of the most common heat set insert sizes used in 3D printed parts. It is widely used in electronics housings, small brackets, fixtures, access covers, service panels, and functional printed assemblies. Because M3 inserts are used so often, installation mistakes are also common: oversized holes, tilted inserts, melted bosses, shallow seating, poor screw alignment, and insert spin after repeated assembly.
This guide explains how to install M3 heat set inserts in 3D printed parts and how installation quality affects pull-out strength, torque resistance, boss cracking, screw alignment, and long-term service reliability.
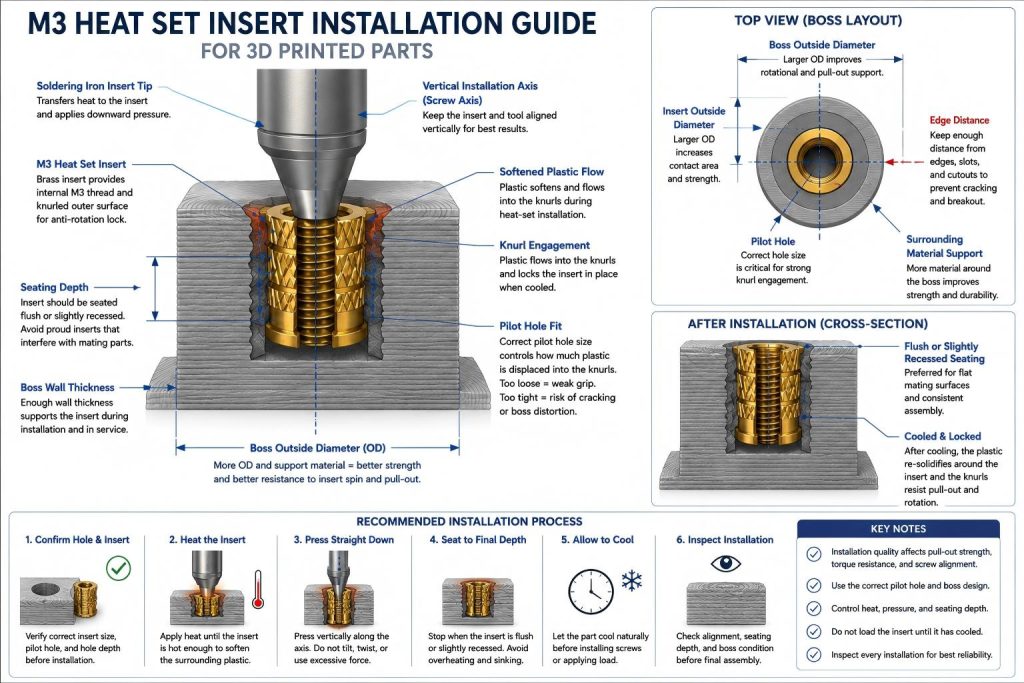
Engineering Overview
Installing an M3 heat set insert means using heat to soften the plastic around the pilot hole so the insert can move into position while its knurls displace and lock into the surrounding material. After cooling, the plastic should grip the insert body and resist both axial pull-out and rotational torque.
The installation process is not separate from part design. A good M3 heat set insert hole size helps the insert enter cleanly. A strong M3 boss design gives the surrounding plastic enough support. The M3 heat set insert dimensions reference helps confirm insert OD, insert length, and hole depth relationship before installation.
If the pilot hole is too loose, the insert may seat easily but have weak retention. If the hole is too tight, the boss may crack, bulge, or deform during installation. If the insert is overheated, the surrounding plastic may melt too much and lose knurl definition. If the insert is pressed at an angle, screw alignment and load transfer both suffer.
Typical Installation Factors for M3 Heat Set Inserts
The table below summarizes the main installation variables. These are engineering starting points, not universal settings. Actual installation behavior depends on insert series, knurl geometry, material, printer calibration, hole tolerance, soldering iron tip shape, heat dwell time, and boss design.
| Installation Variable | Effect on M3 Insert Performance | Risk if Poorly Controlled | Engineering Note |
|---|---|---|---|
| Pilot Hole Diameter | Controls how much plastic flows around the insert knurls | Oversized holes reduce grip; undersized holes can crack the boss | Hole fit should be verified before installing multiple inserts. |
| Hole Depth | Allows full insert seating without bottoming out | Too shallow may leave the insert proud or force plastic upward | Hole depth should account for insert length and any displaced material. |
| Installation Temperature | Softens plastic enough for insert seating | Too cold causes force damage; too hot causes boss melting | Material behavior matters more than a single universal temperature value. |
| Heat Dwell Time | Controls how long the insert transfers heat into the boss | Too short prevents seating; too long weakens the surrounding plastic | Use steady pressure and stop once the insert reaches final depth. |
| Insertion Alignment | Keeps the screw axis straight and distributes load evenly | Tilted inserts cause screw binding, uneven knurl loading, and weak joints | A vertical press or guided soldering tip improves consistency. |
| Seating Depth | Determines whether the insert sits flush, proud, or recessed | Proud inserts interfere with mating parts; shallow inserts reduce engagement | Flush or slightly recessed seating is usually preferred for flat mating surfaces. |
| Boss Wall Thickness | Supports the insert during heating, pressing, cooling, and screw loading | Thin bosses may split, bulge, or soften excessively | Installation quality cannot compensate for a boss that is too weak. |
| Cooling Time | Allows the plastic to re-solidify around the insert | Loading the screw too soon may disturb the insert position | Let the insert cool before applying screw preload or test loads. |
| Post-Installation Inspection | Confirms alignment, seating, and boss condition | Hidden tilt or cracking may only show up during assembly | Inspect before committing to repeated assembly or service use. |
Recommended M3 Installation Process
1. Confirm the Insert and Hole Match
Before installation, confirm the insert size, insert length, outside diameter, and pilot hole. M3 inserts are not all identical. Different insert series may have different outside diameters, knurl patterns, flange shapes, and installation depths.
The pilot hole should be designed around the actual insert geometry, not only the M3 thread size. If the hole was designed from thread diameter alone, the insert may not develop enough pull-out strength or torque resistance.
2. Check the Boss Before Heating
Inspect the boss wall thickness, boss outside diameter, edge distance, and print quality before installing the insert. A boss that is too thin, too close to an edge, or poorly printed may fail even if the insert is installed carefully.
If the boss already looks weak, installation heat and pressure may make the failure worse. For structural design checks, compare the boss geometry with the boss OD ratio and minimum wall thickness references.
3. Use a Controlled Heat Source
A soldering iron with a suitable insert tip is commonly used for M3 heat set insert installation. The tip should contact the insert cleanly and apply heat along the insert axis. Avoid pushing directly with a sharp or uneven tip that can tilt the insert.
The goal is to heat the insert enough for the surrounding plastic to soften and flow into the knurls, not to melt the boss into a large softened zone. Excessive heat can reduce retention because the plastic loses definition around the insert surface.
4. Press Straight Down Along the Screw Axis
The insert should move into the pilot hole vertically. Do not drag, twist, or angle the insert during installation. A tilted insert can cause screw misalignment and uneven knurl engagement, which may reduce both M3 pull-out strength and M3 torque resistance.
If accuracy matters, use a vertical press, installation jig, or guided soldering iron setup instead of freehand installation. Freehand installation can work for prototypes, but it is less consistent across multiple bosses.
5. Stop at the Correct Seating Depth
For most M3 printed assemblies, the insert should be flush or slightly recessed below the boss surface. A proud insert may prevent mating parts from sitting flat. A deeply recessed insert may reduce screw engagement or create assembly stack-up problems.
Do not keep pressing after the insert reaches final depth. Extra heat dwell can over-soften the surrounding plastic and weaken the joint.
6. Let the Insert Cool Before Loading
After installation, allow the insert and surrounding plastic to cool before installing the screw or applying preload. If a screw is installed too soon, the insert may shift, tilt, or disturb the softened plastic around the knurls.
Cooling is especially important in PETG and ABS because these materials may stay soft or flexible longer than expected near the heated insert.
7. Inspect the Installation
After cooling, check that the insert is straight, seated properly, and surrounded by intact plastic. Look for signs of boss cracking, local melting, raised plastic, tilted seating, or edge breakout.
A good M3 installation should allow the screw to enter smoothly without binding. If the screw feels misaligned, the insert may have been installed at an angle or the hole axis may not match the mating part.
Material Adjustments for PLA, PETG, and ABS
PLA
PLA is stiff and can hold a clean insert shape after cooling, but it is also brittle. During M3 insert installation, a hole that is too tight or a boss wall that is too thin may crack rather than deform.
Use controlled heat and avoid forcing the insert. If the insert does not move smoothly, do not simply press harder. Check whether the pilot hole is too small, the boss is too cold, or the insert is misaligned.
PLA often gives a crisp initial lock, but it may fail suddenly if over-tightened after installation. Inspect for stress whitening or fine cracks around the boss.
PETG
PETG is tougher and more ductile than PLA, so it often tolerates heat set installation with less cracking. However, PETG can also become soft and stringy when overheated, which may reduce clean knurl engagement.
For PETG, avoid excessive heat dwell and avoid loading the insert immediately after installation. The joint may feel secure at first but gradually relax if screw preload is high or if the part is used in a warm environment.
PETG M3 inserts usually benefit from good boss support, controlled screw tightening, and enough cooling time before assembly.
ABS
ABS can be a good material for M3 heat set inserts because it tolerates heat and impact better than PLA in many functional applications. However, installation control still matters.
If the iron is too hot or held too long, ABS around the insert may soften excessively and lose mechanical definition. This can reduce pull-out strength and torque resistance after cooling.
ABS parts also depend on print quality and layer adhesion. A poorly printed boss may split along layer lines even if the insert is installed at the right depth.
Common M3 Installation Mistakes
1. Oversized Pilot Hole
An oversized pilot hole may make installation easy, but it reduces plastic displacement into the insert knurls. The result can be weak retention, insert spin, or poor long-term stability.
2. Hole Too Tight
A hole that is too tight can crack the boss, especially in PLA. It may also force the insert to push material outward, creating bulging or raised plastic around the boss.
3. Too Much Heat
Too much heat can melt the boss beyond the insert surface. The insert may sink too easily, tilt, or sit in a softened plastic pocket that does not provide enough mechanical lock after cooling.
4. Too Little Heat
If the insert is not hot enough, it may require excessive pressing force. This can crush the boss, create layer separation, or stop the insert before it reaches full seating depth.
5. Tilted Installation
A tilted insert causes screw misalignment and uneven load transfer. It may still look acceptable from above, but the screw may bind or the insert may spin during repeated use.
6. Shallow Seating
A shallow insert reduces engagement length and may interfere with mating surfaces. It can also concentrate load near the top of the boss instead of distributing it along the insert length.
7. Loading the Insert Too Soon
Installing the screw before the plastic cools can disturb the insert position. This is especially risky when the insert is used for alignment-critical assemblies.
Post-Installation Checks
Installation defects should be checked against M3 heat set insert failure modes.
After installing an M3 heat set insert, check the following before final assembly:
- The insert is flush or slightly recessed.
- The insert axis is straight and aligned with the screw path.
- The surrounding boss is not cracked or heavily melted.
- The screw enters smoothly without cross-threading or binding.
- The boss has enough wall thickness around the insert.
- The insert does not rotate under normal screw tightening.
- The mating part sits flat without interference from a proud insert.
How Installation Affects Pull-Out Strength and Torque Resistance
Installation quality directly affects both axial and rotational performance. Pull-out strength depends on how well the insert engages the plastic along its length, while torque resistance depends on how well the plastic locks around the insert knurls and resists rotation.
A shallow insert may reduce pull-out strength. A loose or overheated insert may reduce torque resistance. A tilted insert may reduce both. Because M3 is often used in serviceable assemblies, even small installation errors can become more visible after repeated screw cycles.
If a joint will be opened and closed many times, installation consistency matters as much as the first test result. A cleanly installed insert is more likely to maintain alignment, preload, and anti-rotation behavior over repeated use.
When M3 Installation Is Usually Reliable
- The pilot hole matches the insert series and printed material.
- The boss has enough outside diameter and wall thickness.
- The insert is heated and pressed along the correct axis.
- The insert is fully seated without excessive heat dwell.
- The plastic is allowed to cool before screw loading.
- The screw tightening torque is controlled.
- The part does not place the insert too close to an unsupported edge.
When M3 Installation Is Likely to Fail
- The pilot hole is oversized or poorly calibrated.
- The boss wall is too thin for the insert OD.
- The insert is forced into cold or underheated plastic.
- The insert is overheated and sinks into a melted pocket.
- The insert is installed at an angle.
- The boss is printed with weak layer adhesion.
- The screw is tightened before the insert cools.
- The assembly requires more torque or pull-out strength than M3 can provide.
Related Engineering Guides
- M3 Heat Set Insert Dimensions Reference
- M3 Heat Set Insert Hole Size for 3D Printed Parts
- M3 Heat Set Insert Boss Design for 3D Printed Parts
- M3 Heat Set Insert Pull-Out Strength for 3D Printed Parts
- M3 Heat Set Insert Torque Resistance for 3D Printed Parts
- Heat Set Insert Installation Temperature for 3D Printed Parts
- Heat Set Insert Hole Depth Chart for 3D Printed Parts
- Heat Set Insert Seating Depth Reference for 3D Printed Parts
- Heat Set Insert Pilot Hole Tolerance Reference for 3D Printed Parts
- PLA vs PETG vs ABS for Threaded Inserts
FAQ
How do you install M3 heat set inserts in 3D printed parts?
Install M3 heat set inserts by using a properly sized pilot hole, heating the insert with a controlled soldering iron or insert tip, pressing it straight into the boss, stopping at the correct seating depth, and allowing the plastic to cool before screw loading.
Why does an M3 heat set insert tilt during installation?
An M3 insert may tilt if the pilot hole is misaligned, the soldering iron tip is not centered, the insert is pushed at an angle, or the boss softens unevenly during heating.
Should an M3 heat set insert sit flush or recessed?
For most 3D printed assemblies, an M3 insert should sit flush or slightly recessed. A proud insert may interfere with mating surfaces, while an overly recessed insert may reduce screw engagement or create stack-up problems.
Why does an M3 insert spin after installation?
An M3 insert may spin after installation if the pilot hole was oversized, the insert was overheated, the knurls did not engage enough plastic, the boss wall was too thin, or the screw was tightened beyond what the printed boss could resist.
Can the same M3 installation settings be used for PLA, PETG, and ABS?
No. PLA, PETG, and ABS respond differently to heat and pressure. PLA is stiffer but more brittle, PETG is tougher but may relax, and ABS can handle heat better but still needs controlled installation.
Related Decision Resources
For insert selection, tool choice, and supplier comparison, use these decision-focused references after the engineering requirements are defined.