
Heat Set Inserts for 3D Printed Linear Rail End Stops are used when a printed block, bracket, or stop feature needs reusable screw threads for limiting carriage travel, adjusting stop position, holding bumper hardware, or fastening a stop block to a rail-mounted assembly.
Linear rail end stops are not loaded like simple covers or static brackets. They may see repeated impact, vibration, screw adjustment, and concentrated force when a carriage reaches the end of travel. This makes insert placement, boss geometry, wall thickness, screw engagement, and load direction especially important.
Heat set inserts can improve serviceability in printed end stops, but the surrounding printed structure must be designed to resist impact load and repeated adjustment without cracking, spinning, or losing preload.
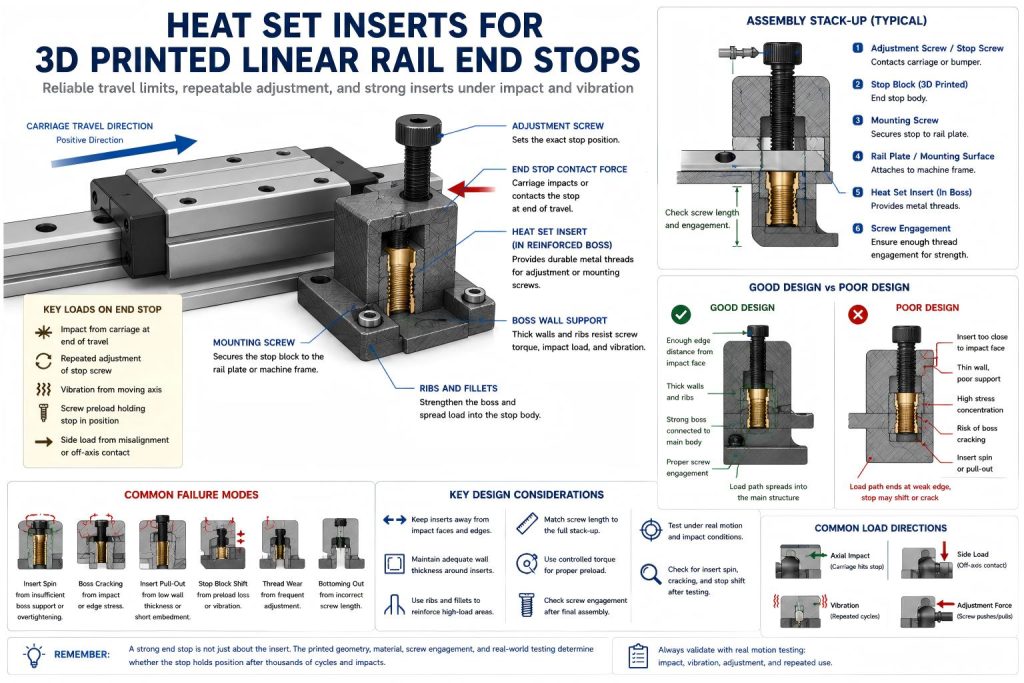
Why Linear Rail End Stops Need Careful Insert Design
A linear rail end stop may look like a small printed block, but it often carries a real mechanical load. When a carriage, slider, or moving axis reaches the end of travel, the stop may receive impact force or repeated contact force.
If the stop uses heat set inserts for adjustment screws, mounting screws, or bumper retention, the insert must resist more than simple screw tightening. It may need to hold position after repeated impacts, vibration, and adjustment cycles.
A weak insert boss can lead to screw loosening, insert spin, stop position drift, or cracking around the mounting hole.
Common Use Cases
3D printed linear rail end stops appear in prototypes, fixtures, CNC accessories, robotics systems, test rigs, printer modifications, and small machine assemblies.
- linear rail carriage travel stops
- adjustable stop screw blocks
- end-stop brackets for small motion systems
- bumper mounting blocks
- limit switch striker blocks
- fixture slide stops
- robotic axis travel limit blocks
- prototype machine rail stops
For related mechanical applications, see Heat Set Inserts for High-Vibration Motor Mounting Brackets and Heat Set Inserts for Printed Jigs with Replaceable Wear Plates.
How End Stop Loads Affect Inserts
End stops often see loads that are directional and repeated. A screw may hold the stop block in place, while another screw may act as an adjustable contact point. The insert can experience torque, axial pull, side load, and vibration.
Common load types include:
- carriage impact at the end of travel
- repeated contact against an adjustment screw
- vibration from a moving axis
- side load from misaligned motion
- screw preload holding the stop to a rail plate
- pull-out load from a bumper or contact screw
- repeated screw adjustment during calibration
The insert should be placed so the printed material carries these loads through a supported path, not through a thin tab or weak edge.
Insert Placement in Linear Rail End Stops
Insert placement should follow the direction of load. If the moving carriage hits the stop from one side, the insert boss should not be placed so close to that side that the load cracks through the wall.
A common mistake is placing a threaded insert near the end of a narrow printed block because the screw location looks convenient. Under repeated contact, the thin wall between the insert and the end face may crack or deform.
Good placement usually means:
- enough distance between the insert and the impact face
- enough wall thickness around the insert hole
- boss support connected to the main body of the stop
- ribs or fillets behind high-load areas
- avoiding inserts in thin unsupported tabs
- aligning screw force with a strong printed load path
For geometry limits, see Heat Set Insert Edge Distance Reference for 3D Printed Parts and Heat Set Insert Minimum Wall Thickness Reference for 3D Printed Parts.
Adjustment Screws and Insert Wear
Many linear rail end stops use adjustment screws to set the exact stop position. This is a strong use case for heat set inserts because the screw may be turned many times during calibration.
Printed plastic threads can wear quickly under repeated adjustment. A brass heat set insert provides more durable internal threads, but the insert must still be supported by the printed body. If the adjustment screw is loaded by impact, the insert may experience repeated axial or bending stress.
For screw engagement behavior, see Screw Engagement Length for Heat Set Inserts in 3D Printed Parts.
Mounting Inserts vs Adjustment Inserts
Linear rail end stops may use inserts in different ways. Some inserts hold the stop block to a base plate or rail carriage. Other inserts hold an adjustment screw, bumper, or limit screw.
| Insert Role | Main Load | Design Priority |
|---|---|---|
| Mounting insert | Screw preload holding the stop block in position | Prevent loosening, pull-out, and boss cracking. |
| Adjustment insert | Repeated screw rotation and contact load | Maintain thread durability and screw position. |
| Bumper insert | Impact or compression through rubber or plastic bumper | Distribute load into the printed body. |
| Limit switch striker insert | Small repeated contact force | Maintain alignment and avoid screw drift. |
Each insert role may need a different boss layout, screw length, torque, and material choice.
Boss Design for End Stop Blocks
A linear rail end stop should avoid concentrating load around a small unsupported insert boss. The boss should be connected to the main body of the stop so the load can spread into the printed part.
Useful boss design features include:
- large enough boss outside diameter
- adequate wall thickness around the insert
- ribs behind the insert boss
- fillets at boss-to-body transitions
- solid material behind impact faces
- enough depth for insert length and screw engagement
- print orientation that resists splitting under the load direction
For boss design, see How to Design Bosses for Heat Set Inserts and Boss OD Ratio for Heat Set Inserts in 3D Printed Parts.
Torque and Preload in End Stop Assemblies
Overtightening a screw in a rail end stop can crack the boss or spin the insert. Undertightening can allow the stop block to shift after repeated carriage contact.
The tightening torque should be enough to keep the stop stable but not so high that the printed boss becomes the failure point. This is especially important in PETG, nylon, or other materials that can relax under load.
For tightening guidance, see Heat Set Insert Torque Range Reference for 3D Printed Parts.
Assembly Stack-Up and Bottoming Out
End stop assemblies may include the printed stop block, rail plate, washer, screw head, insert, adjustment screw, or bumper hardware. If the screw is too long, it may bottom out before clamping the assembly. If the screw is too short, it may not engage enough insert thread.
Stack-up should be checked with the final screw, washer, rail plate, and stop block thickness. A screw that feels tight may actually be bottoming out instead of creating real preload.
For stack-up planning, see Heat Set Insert Assembly Stack-Up Reference for 3D Printed Parts.
Material Considerations
Material choice affects how the end stop handles impact, vibration, and screw preload. PLA may be stiff but brittle under repeated impact. PETG may absorb some load but creep over time. ABS and ASA may handle temperature better. Nylon may tolerate impact but may relax under sustained preload.
| Material | End Stop Behavior | Insert Design Note |
|---|---|---|
| PLA | Stiff, but brittle under repeated impact | Use generous boss support and avoid thin stop faces. |
| PETG | Tougher, but prone to preload relaxation | Check stop shift and screw loosening after cycling. |
| ABS | Better impact and temperature behavior | Check layer adhesion near bosses and impact faces. |
| ASA | Useful for exposed mechanical assemblies | Maintain edge distance and avoid sharp stress paths. |
| Nylon | Good toughness and impact tolerance | Check long-term screw preload and dimensional stability. |
| Fiber-filled materials | Stiff and dimensionally stable | Avoid brittle cracking near insert bosses and impact faces. |
For material comparison, see PLA vs PETG vs ABS for Threaded Inserts.
Common Failure Modes
Linear rail end stops usually fail when the repeated stop load is transferred into weak printed geometry around the insert.
- insert spin during adjustment screw tightening
- boss cracking near the impact face
- insert pull-out from repeated contact load
- stop block shifting after vibration
- screw preload loss after repeated impacts
- thread wear from frequent adjustment
- rail stop cracking along layer lines
- bottoming out from incorrect screw length
For related failure explanations, see Why Do Heat Set Inserts Fail Under Vibration? and Why Does Screw Preload Drop in 3D Printed Insert Joints?.
Testing Linear Rail End Stops
On moving-axis assemblies, cable chain mounting brackets create a related vibration and alignment fastening case.
Nearby motion systems often use limit switch mounts with similar repeat-positioning and vibration requirements.
A rail end stop should be tested in the real direction of travel. Installing an insert successfully is not enough. The end stop must hold position after repeated contact and adjustment.
A useful test should include:
- installing inserts in the final print orientation
- assembling the stop with the real screw and washer
- checking screw engagement and bottom clearance
- applying repeated carriage contact or controlled impact
- adjusting the stop screw multiple times
- checking whether the insert spins or loosens
- checking whether the stop block shifts position
- inspecting boss walls and layer lines for cracks
Design Checklist
- Place inserts away from thin impact faces and weak edges.
- Use enough wall thickness around the insert body.
- Connect insert bosses to the main stop body with ribs or thick geometry.
- Use fillets near boss transitions and impact surfaces.
- Match screw length to the final stack-up.
- Use controlled torque to avoid insert spin or boss cracking.
- Check adjustment screw engagement after repeated use.
- Choose material based on impact, vibration, temperature, and creep behavior.
- Test the end stop in the real direction of carriage travel.
FAQ
Are heat set inserts useful for 3D printed linear rail end stops?
Yes. They are useful when the stop block needs reusable threads for adjustment screws, mounting screws, or bumper hardware. The printed boss must still be designed to resist impact and repeated adjustment.
Where should inserts be placed in a rail end stop?
Inserts should be placed away from thin impact faces, sharp corners, and weak edges. The boss should connect to the main stop body so load can spread through the printed structure.
Can a heat set insert hold an adjustable stop screw?
Yes, if the insert has enough support and the screw engagement is adequate. Adjustment screws may be turned repeatedly, so thread durability and insert stability are important.
What causes end stop inserts to loosen?
Common causes include vibration, repeated impact, poor screw engagement, oversized pilot holes, weak boss geometry, preload loss, and material creep.
Should rail end stops be tested under real motion?
Yes. The end stop should be tested in the actual carriage travel direction with the final screw, washer, material, and adjustment condition.
Related Guides
- Heat Set Insert Edge Distance Reference for 3D Printed Parts
- Heat Set Insert Minimum Wall Thickness Reference for 3D Printed Parts
- Boss OD Ratio for Heat Set Inserts in 3D Printed Parts
- Heat Set Insert Torque Range Reference for 3D Printed Parts
- Heat Set Insert Assembly Stack-Up Reference for 3D Printed Parts
- Screw Engagement Length for Heat Set Inserts in 3D Printed Parts
- Why Do Heat Set Inserts Fail Under Vibration?
- Why Does Screw Preload Drop in 3D Printed Insert Joints?