
If your M4 heat set inserts are spinning, cracking PLA, or failing under load in 3D printed parts, the most common cause is incorrect hole size or poor tolerance control.
This guide explains the recommended M4 hole size for PLA and PETG materials.
M4 heat set insert hole size for 3D printed parts depends on the insert’s outer diameter, knurl geometry, printed material, hole depth, boss wall thickness, and how much plastic displacement is needed during installation.
An M4 insert is larger than the common M3 size, so the pilot hole is not just a scaled-up detail. A larger insert displaces more plastic, stores more heat, and applies more radial pressure to the printed boss during installation. For this reason, M4 hole sizing needs more attention to boss support, wall thickness, and insertion control.
This guide explains how to think about M4 heat set insert hole size in 3D printed parts without treating any single number as universal. Always check the insert manufacturer’s drawing first, then adjust based on material, print tolerance, boss geometry, and test fitting.
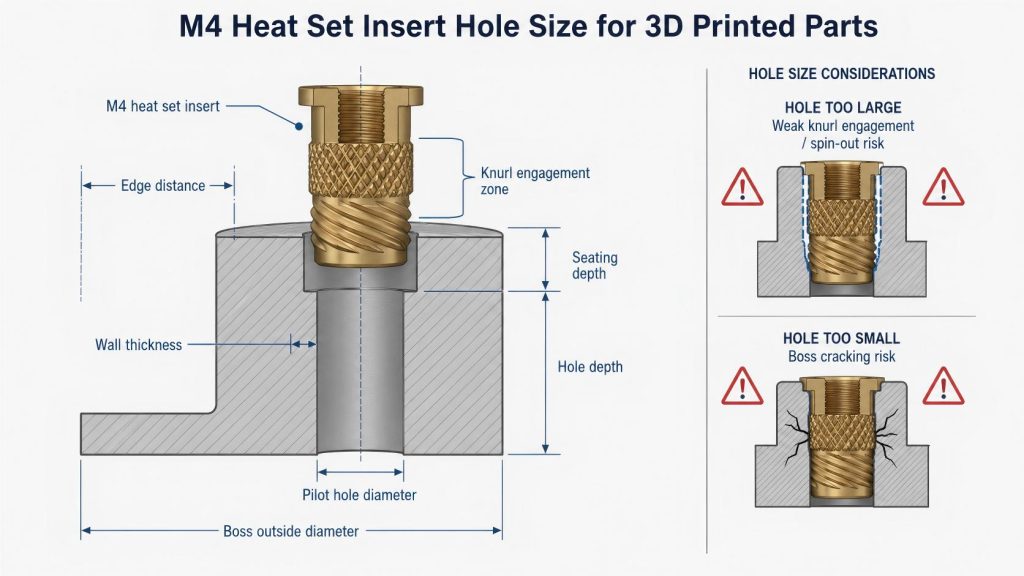
What Is the Recommended Hole Size for an M4 Heat Set Insert?
There is no single universal hole size for every M4 heat set insert because insert outer diameters vary by manufacturer, knurl pattern, length, and flange design. The correct starting point is the manufacturer’s recommended pilot hole diameter for the exact insert being used.
For 3D printed parts, the pilot hole should usually be slightly smaller than the insert’s outer knurled diameter so the heated brass insert can displace softened plastic and create mechanical grip around the knurl features.
If the hole is too large, the insert may not develop enough plastic engagement. If the hole is too small, insertion pressure may crack the boss, distort the surrounding wall, or push excess molten plastic into the bottom of the hole.
Why M4 Hole Size Needs More Care Than M3
M4 inserts are often used in stronger printed assemblies, brackets, fixtures, mounting plates, and serviceable structural parts. Compared with M3 inserts, they usually involve higher screw torque, larger bosses, deeper holes, and greater clamp load.
This means the hole size must support both installation and service conditions:
- The hole must allow the insert to enter without excessive boss cracking.
- The softened plastic must flow into the insert knurl pattern.
- The boss must have enough wall thickness to resist radial expansion.
- The final seated insert must remain aligned with the screw axis.
- The surrounding material must support tightening torque and repeated use.
A hole size that works in a thick fixture block may be too aggressive for a thin mounting tab. A hole size that works in PETG may split a thin PLA boss if the boss geometry is weak.
Key Variables That Affect M4 Heat Set Insert Hole Size
M4 pilot hole size should be selected together with the surrounding geometry. The hole does not work alone.
| Variable | Why It Matters |
|---|---|
| Insert outer diameter | The knurled outer diameter defines the basic pilot hole range. |
| Insert length | Longer inserts require enough hole depth and more controlled heat transfer. |
| Knurl geometry | Aggressive knurls need enough plastic flow but may increase insertion pressure. |
| Printed material | PLA, PETG, ABS, ASA, and nylon soften, creep, and crack differently. |
| Boss outside diameter | A larger M4 insert needs enough surrounding plastic to resist splitting. |
| Wall thickness | Thin walls around an M4 insert increase cracking and deformation risk. |
| Hole depth | Insufficient depth can cause bottoming, proud inserts, or poor seating. |
| Print tolerance | Printed holes often come out smaller or less round than the CAD value. |
| Insertion temperature | Too little heat increases force; too much heat can soften the surrounding boss. |
M4 Hole Size Is Not Only a Diameter Problem
For M4 heat set inserts, pilot hole diameter is only one part of the fastening structure. A larger insert can create more useful thread engagement, but it also places more demand on the printed boss.
The hole should be evaluated together with:
- Boss outside diameter
- Minimum wall thickness around the insert
- Edge distance from the insert to the nearest wall or corner
- Hole depth and insert seating depth
- Screw engagement length
- Expected tightening torque
- Whether the part will be assembled repeatedly
If the surrounding geometry is weak, simply increasing insert size from M3 to M4 may create a larger failure instead of a stronger joint.
Hole Too Large: Common M4 Insert Problems
If the M4 pilot hole is too large, the heated insert may enter easily but fail to develop enough mechanical grip after cooling.
Possible symptoms include:
- The insert pushes in with very little resistance.
- The insert can rotate during screw tightening.
- The screw tightens at first but loses torque during service.
- The insert pulls out under axial load.
- The surrounding plastic does not visibly engage the knurl pattern.
A hole that is too large often reduces torque resistance and pull-out strength because the softened plastic does not flow tightly enough into the insert’s external features.
Hole Too Small: Common M4 Insert Problems
If the M4 pilot hole is too small, the insert may require too much force during installation. Because M4 inserts displace more plastic than smaller inserts, an undersized hole can create strong radial pressure in the boss.
Possible symptoms include:
- The boss cracks during insertion.
- The insert stops before reaching full depth.
- Molten plastic bulges around the top of the hole.
- The insert tilts because force is not balanced.
- The part surface deforms around the boss.
- Thin walls split along layer lines.
This risk is especially important in PLA, thin bosses, edge locations, and parts with limited wall support.
Material Considerations for M4 Heat Set Insert Holes
PLA
PLA can hold sharp printed geometry, but it is less forgiving when radial stress is high. For M4 inserts, an overly tight pilot hole or thin boss may cause cracking during installation. PLA boss design should be conservative, with enough wall thickness and controlled insertion pressure.
PETG
PETG is generally more ductile than PLA, but it may deform or creep under sustained load. For M4 inserts, the hole should allow good knurl engagement without overheating the surrounding plastic. PETG parts used in service covers or repeated assembly should also be evaluated for long-term preload loss.
ABS and ASA
ABS and ASA can be more heat-tolerant than PLA and PETG, but print settings, layer adhesion, and part geometry still matter. M4 inserts in ABS or ASA should still be test-fitted because printed hole size and boss support can vary significantly.
Nylon and Filled Materials
Nylon and filled materials may behave differently depending on fiber content, moisture, and print settings. M4 heat set insert holes in these materials should be validated with test parts because heat transfer, plastic flow, and retention may not match PLA or PETG behavior.
Blind Holes vs Through Holes for M4 Inserts
M4 heat set inserts are often used in thicker printed parts, so blind holes are common. A blind hole must be deep enough for the full insert length plus displaced plastic and any installation tolerance.
If a blind hole is too shallow, the insert may bottom out before seating properly. This can leave the insert proud of the surface, reduce screw engagement, or force molten plastic into unwanted areas.
Through holes can reduce bottoming risk, but they may allow molten plastic or the insert to pass beyond the intended seating position if installation is not controlled.
Boss Geometry Around M4 Heat Set Insert Holes
An M4 hole should not be placed in a weak boss or thin wall without enough surrounding plastic. Because M4 inserts are larger and often used with higher tightening loads, boss design is critical.
Review the following before choosing the final hole size:
- Is the boss outside diameter large enough for the insert?
- Is there enough wall thickness around the hole?
- Is the insert too close to an edge, slot, corner, or thin wall?
- Will the screw apply bending, pull-out, or vibration load?
- Will the part be repeatedly opened and closed?
If the boss is too small, even a correct pilot hole diameter may not prevent cracking or long-term loosening.
Recommended Design Process for M4 Pilot Holes
- Start with the exact insert manufacturer’s pilot hole recommendation.
- Confirm the insert’s outer knurled diameter and length.
- Check printed hole accuracy with your printer, material, and slicer settings.
- Print a small test boss or test coupon before committing to the final part.
- Install the insert using controlled heat and steady vertical pressure.
- Check whether the insert seats flush, remains aligned, and resists rotation.
- Adjust the CAD hole only after checking the actual printed result.
- Validate the design under the expected screw torque and assembly cycle conditions.
When to Choose M4 Instead of M3
M4 inserts may be appropriate when the printed part needs more screw engagement, higher clamp load, greater torque resistance, or stronger fastening than an M3 insert can reasonably provide.
Common M4 use cases include:
- Printed brackets
- Mounting plates
- Machine guards
- Fixtures and jigs
- Motor or actuator mounts
- Structural prototype assemblies
- Serviceable covers that need stronger screws
However, M4 should not be chosen only because it seems stronger. The printed part must have enough geometry to support the larger insert.
Common Mistakes With M4 Heat Set Insert Hole Size
- Using a generic M4 hole size without checking the insert drawing.
- Assuming all M4 heat set inserts have the same outer diameter.
- Copying an M3 hole strategy without increasing boss support.
- Making the pilot hole too tight in PLA.
- Using M4 inserts too close to part edges.
- Ignoring printed hole shrinkage or ovality.
- Using a blind hole that is too shallow.
- Overheating the boss during installation.
- Testing only fit, but not screw torque or repeated assembly behavior.
Related Engineering Guides
- Heat Set Insert Hole Size Guide
- M3 Heat Set Insert Hole Size for 3D Printed Parts
- How to Design Bosses for Heat Set Inserts
- M3 Heat Set Insert Boss Design for 3D Printed Parts
- PLA vs PETG vs ABS for Threaded Inserts
- Torque Resistance of Heat Set Inserts in 3D Printed Parts
Related Engineering References
- M4 Heat Set Insert Dimensions Reference for 3D Printed Parts
- Heat Set Insert Hole Depth Chart for 3D Printed Parts
- Heat Set Insert Pilot Hole Tolerance Reference for 3D Printed Parts
- Heat Set Insert Minimum Wall Thickness Reference for 3D Printed Parts
- Heat Set Insert Seating Depth Reference for 3D Printed Parts
Conclusion
M4 heat set insert hole size should be selected from the exact insert drawing, then validated in the printed material and boss geometry used in the real part. A correct M4 pilot hole is not only about diameter. It must also work with boss wall thickness, hole depth, material behavior, installation heat, screw torque, and the expected service load.
For structural 3D printed parts, the safest approach is to treat the M4 pilot hole as part of the complete fastening structure rather than as an isolated number.
FAQ
What is the correct hole size for M4 heat set inserts?
✔ Answer:
For most M4 heat set inserts, the recommended hole size is typically 4.6 mm to 4.8 mm, depending on material (PLA or PETG) and insert geometry.
If the hole is too large, the insert may spin under load. If it is too small, it may crack PLA during installation. Incorrect sizing can also reduce long-term strength and durability.
Related Decision Resources
For insert selection, tool choice, and supplier comparison, use these decision-focused references after the engineering requirements are defined.