
M5 heat set insert pull-out strength for 3D printed parts depends on insert length, knurl engagement, pilot hole fit, boss wall thickness, boss base support, material behavior, print orientation, hole depth, installation quality, and how the load is transferred into the printed part.
M5 inserts can provide strong fastening in large 3D printed parts, but the larger screw size does not automatically create a stronger joint. Pull-out strength is controlled by the complete fastening structure: the brass insert, the softened plastic around the knurls, the printed boss, the layer direction, and the load path into the part body.
This guide explains how to evaluate M5 heat set insert pull-out strength without assuming that insert size alone determines joint strength.
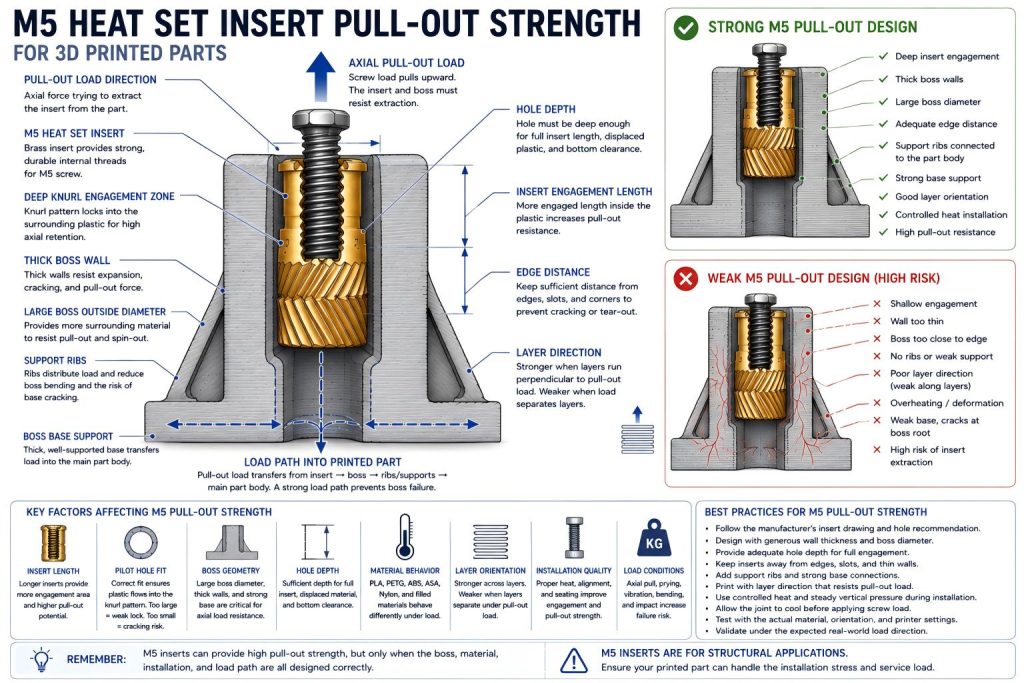
What Pull-Out Strength Means for M5 Heat Set Inserts
Pull-out strength describes the resistance of the insert against being extracted from the printed part along the screw axis. In an M5 heat set insert joint, pull-out failure may happen under axial screw tension, prying force, bracket load, vibration, repeated assembly, or overloaded structural fastening.
M5 inserts are often used in fixture bodies, machine panels, large brackets, mounting blocks, service covers, equipment housings, and prototype structures. These applications may demand more from the printed boss than small enclosure screws or light covers.
A strong M5 joint requires more than a large brass insert. It requires a printed structure that can carry the load.
Why M5 Pull-Out Strength Depends on the Printed Boss
M5 inserts are larger than M2, M3, and M4 inserts. They usually have more surface area, more insert length, and more screw engagement potential. However, the larger insert also creates more installation stress and requires more surrounding support.
Pull-out strength depends on whether the boss can provide:
- Enough wall thickness around the insert
- Enough hole depth for full insert engagement
- A strong boss base connected to the main part body
- A pilot hole that allows proper knurl engagement
- Good layer orientation relative to the pull-out load
- Enough edge distance from slots, corners, and thin walls
- Controlled installation heat to avoid weakening the boss
If the printed boss cannot support the insert, an M5 insert may pull out, crack the boss, spin inside the plastic, or tear out a larger damaged area.
Main Variables That Affect M5 Pull-Out Strength
| Variable | Effect on Pull-Out Strength |
|---|---|
| Insert length | Longer inserts can provide more engagement area, but only if the boss is deep and strong enough. |
| Knurl geometry | External features help lock the insert into the surrounding plastic. |
| Pilot hole size | Controls plastic displacement and mechanical grip around the insert body. |
| Hole depth | Must allow full insert seating without bottoming or losing screw engagement. |
| Boss outside diameter | Provides surrounding material to resist expansion, cracking, and extraction. |
| Wall thickness | Thin walls reduce the amount of plastic available to hold the insert. |
| Boss base support | Controls whether pull-out load transfers into the part body or breaks the boss base. |
| Material | PLA, PETG, ABS, ASA, nylon, and filled materials differ in cracking, creep, and layer adhesion. |
| Print orientation | Layer direction affects whether the boss resists pull-out or separates along layer lines. |
| Installation quality | Tilted, overheated, underheated, or poorly seated inserts usually reduce strength. |
| Load direction | Axial pull, prying, shear, bending, and vibration create different failure risks. |
M5 Pull-Out Strength Is Not Only About Insert Size
A common design mistake is assuming that M5 automatically solves pull-out strength problems because it is larger than M3 or M4. A larger insert can help only when the printed part has enough geometry to use that extra engagement area.
If the boss is thin, close to an edge, shallow, unsupported, or printed in a weak orientation, the M5 insert may not reach its potential strength. The failure may simply become larger and more destructive.
The better question is:
Can the printed boss, material, and load path support the pull-out force expected from an M5 joint?
How Pilot Hole Size Affects M5 Pull-Out Strength
Pilot hole size controls how the heated insert displaces softened plastic into the knurl pattern. For M5 inserts, the hole must balance grip and installation stress.
If the pilot hole is too large, the insert may not lock into the plastic strongly enough. If the pilot hole is too small, the insert may crack the boss or require excessive heat and force.
Oversized-hole risks include:
- Weak knurl engagement
- Reduced axial retention
- Insert movement after cooling
- Spin-out under screw torque
- Pull-out under service load
- Loose joint behavior after repeated assembly
Undersized-hole risks include:
- Boss cracking during insertion
- Excessive radial pressure
- Insert tilt
- Plastic bulging near the seating surface
- Incomplete insertion depth
- Overheating while trying to force the insert into place
How Boss Geometry Affects M5 Pull-Out Strength
Boss geometry is often the limiting factor in M5 pull-out strength. The boss must hold the insert and transfer axial load into the surrounding printed part.
Important boss features include:
- Boss outside diameter
- Wall thickness around the insert
- Hole depth
- Boss height
- Boss base thickness
- Fillets at boss transitions
- Support ribs aligned with the load path
- Distance from the insert to nearby edges or corners
A tall, isolated boss may fail at its base even when the insert stays locked inside the boss. A boss with strong base support and ribs can distribute load more effectively into the main part body.
Material Behavior and M5 Pull-Out Strength
PLA
PLA can be stiff and dimensionally stable, but it can crack when the M5 insert creates high radial pressure or when the pull-out load opens a brittle boss structure. PLA M5 bosses should use generous wall support, good edge distance, and controlled insertion heat.
PETG
PETG is more ductile than PLA, which may help during insertion, but it may deform or creep under sustained clamp load. M5 inserts in PETG should be evaluated for long-term preload retention and repeated assembly behavior.
ABS and ASA
ABS and ASA may handle heat better than PLA and PETG, but M5 pull-out behavior still depends on layer adhesion, boss support, print quality, and installation control.
Nylon and Fiber-Filled Materials
Nylon and fiber-filled materials may offer toughness, but their M5 pull-out behavior depends on fiber content, moisture, print settings, and layer bonding. Test coupons or real part prototypes are recommended for high-load applications.
Print Orientation and Layer Direction
Print orientation strongly affects M5 heat set insert pull-out strength. If the pull-out load separates layers, the boss may fail by layer splitting before the insert fully loses grip.
Review whether:
- The insert axis is parallel or perpendicular to layer lines
- The boss base is printed as continuous material
- The screw load opens a weak layer path
- Ribs and support pads align with the load direction
- The part will experience vibration, prying, or repeated assembly
For large insert joints, poor layer direction can turn a strong-looking boss into a weak fastening point.
Installation Quality and Pull-Out Strength
M5 inserts require more heat and transfer more thermal energy into the printed part than smaller inserts. Poor installation can significantly reduce pull-out strength.
Installation problems that reduce strength include:
- Insert installed at an angle
- Insert not seated fully
- Boss overheated during installation
- Insert forced into an undersized hole
- Plastic pushed into the bottom of a blind hole
- Insert sinking too deep
- Large surface bulging around the insert
- Loading the screw before the plastic has cooled
For M5 inserts, heat control and alignment are part of strength design, not just assembly details.
Load Direction and M5 Pull-Out Risk
M5 inserts are often used in parts that see more than simple axial screw tension. Real applications may include prying, bending, vibration, or impact-like loads.
Common load conditions include:
- Axial pull from screw tension
- Prying load from a bracket or cover
- Shear load from mounted hardware
- Bending load at the boss base
- Vibration from motors or moving equipment
- Repeated opening and closing of service panels
- Clamp load from a structural assembly
A joint that survives simple hand tightening may still fail under bending or vibration if the boss base and load path are weak.
Short vs Long M5 Inserts
Longer M5 inserts may improve pull-out resistance by increasing engagement area, but only if the printed boss has enough depth and support.
A longer insert can create problems if:
- The blind hole is too shallow
- The boss wall is too thin
- The insert bottoms out before seating
- The screw stack-up conflicts with the insert depth
- The installation overheats too much surrounding plastic
- The boss base cannot transfer the larger load
Longer inserts are not automatically stronger. They must match the boss geometry and service load.
How to Improve M5 Heat Set Insert Pull-Out Strength
- Use the manufacturer’s insert drawing as the starting point.
- Select an insert length that matches the boss depth and screw engagement needs.
- Use a pilot hole that supports knurl engagement without cracking the boss.
- Increase boss outside diameter when space allows.
- Use enough wall thickness around the insert.
- Keep the insert away from edges, slots, and thin walls.
- Add ribs or a local pad to strengthen the boss base.
- Review print orientation relative to pull-out load.
- Install with controlled heat and vertical alignment.
- Test the joint under the real load direction, not only screw fit.
Common M5 Pull-Out Strength Mistakes
For the adjacent rotational failure mode, see M5 torque resistance.
- Assuming M5 is automatically strong enough because it is large.
- Using a large insert in a thin or unsupported boss.
- Ignoring edge distance and boss base support.
- Using a pilot hole that is too loose for knurl engagement.
- Cracking the boss with an undersized pilot hole.
- Overheating the boss during installation.
- Using a blind hole that is too shallow for a long insert.
- Ignoring screw torque, prying load, or vibration.
- Testing only insertion fit instead of pull-out behavior.
- Using M5 where a through-bolt or metal backing plate would be safer.
When M5 Pull-Out Strength May Not Be Enough
M5 heat set inserts can be useful in stronger printed assemblies, but they may not be enough for safety-critical loads, high impact, severe vibration, heavy prying, or high-temperature service.
Consider alternatives when:
- The printed boss cannot be made large enough
- The insert must sit near a thin edge
- The load is safety-critical
- The joint carries repeated vibration
- The material creeps under clamp load
- The screw load creates strong bending at the boss base
- A metal load path would be more reliable
Alternatives may include through-bolts, metal backing plates, captured nuts, multiple smaller fasteners, larger mounting pads, or hybrid printed-metal structures.
Recommended M5 Pull-Out Design Process
- Select M5 only when the part has enough geometry for a large insert.
- Check the insert drawing for outer diameter, length, and pilot hole recommendation.
- Design the boss with enough outside diameter, wall thickness, and hole depth.
- Check edge distance, boss base support, and ribs.
- Review print orientation relative to pull-out load.
- Print a test boss or prototype in the final material and orientation.
- Install the insert with controlled heat and vertical pressure.
- Inspect for cracking, tilt, proud seating, overheating, or plastic bulging.
- Test screw torque and pull-out behavior under realistic loading.
- Use through-bolts or reinforcement if the printed boss is the weak point.
Related Engineering Guides
- M5 Heat Set Insert Hole Size for 3D Printed Parts
- M5 Heat Set Insert Boss Design for 3D Printed Parts
- M4 Heat Set Insert Pull-Out Strength for 3D Printed Parts
- M3 Heat Set Insert Pull-Out Strength for 3D Printed Parts
- Pull-Out Strength of Heat Set Inserts in 3D Printed Parts
- Layer Adhesion and Heat Set Insert Strength in 3D Printed Parts
- Heat Set Insert Installation Temperature for 3D Printed Parts
Related Engineering References
- M5 Heat Set Insert Dimensions Reference for 3D Printed Parts
- Boss OD Ratio for Heat Set Inserts in 3D Printed Parts
- Heat Set Insert Minimum Wall Thickness Reference for 3D Printed Parts
- Heat Set Insert Edge Distance Reference for 3D Printed Parts
- Heat Set Insert Hole Depth Chart for 3D Printed Parts
- Heat Set Insert Assembly Stack-Up Reference for 3D Printed Parts
Conclusion
M5 heat set insert pull-out strength depends on the full fastening structure. Insert size, insert length, pilot hole fit, knurl engagement, boss wall thickness, boss base support, print orientation, material behavior, installation heat, and load direction all affect the final result.
For large 3D printed parts, M5 inserts can create strong joints only when the printed boss and load path are designed to support them. A large insert in a weak boss is not a strong fastening structure. It is just a larger failure point waiting for load.
Related Decision Resources
For insert selection, tool choice, and supplier comparison, use these decision-focused references after the engineering requirements are defined.