
M5 heat set insert torque resistance depends on how well the insert, pilot hole, boss geometry, wall thickness, boss base, printed material, and screw tightening load work together to prevent insert rotation inside a 3D printed part.
M5 inserts are used when a printed assembly needs stronger fastening than smaller insert sizes such as M2.5, M3, or M4. However, the larger screw size also introduces higher tightening torque, higher preload, more installation heat, and greater stress around the printed boss. For this reason, M5 torque resistance is not only an insert selection issue. It is a structural design issue.
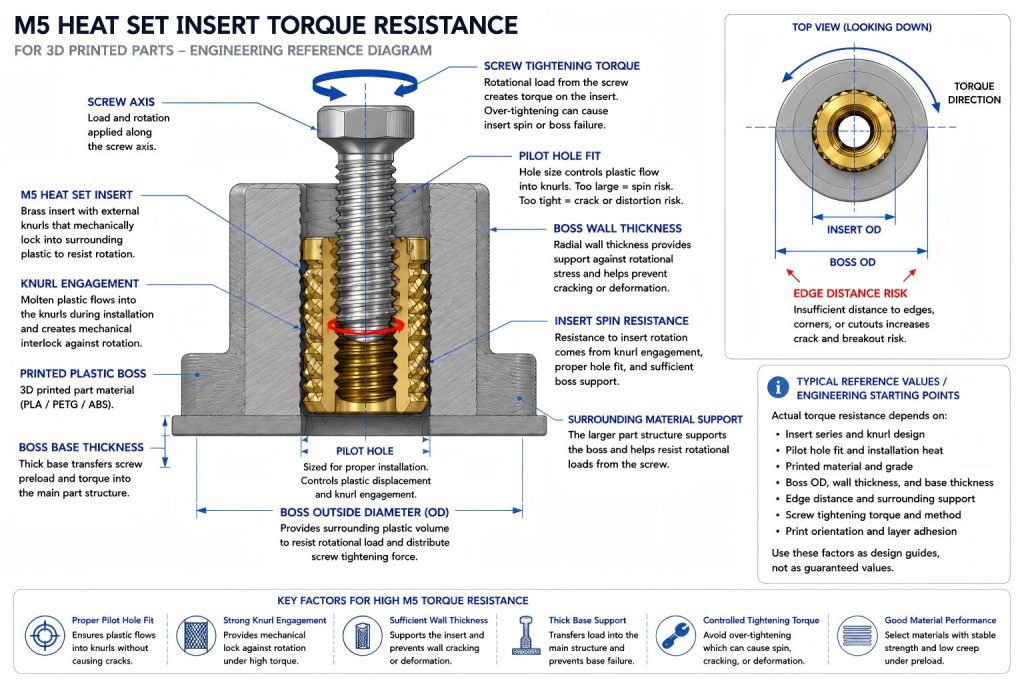
This article explains the engineering factors that affect M5 heat set insert torque resistance in 3D printed parts, including insert spin, boss wall support, pilot hole fit, screw tightening torque, material behavior, and common torque-related failure modes.
Engineering Overview
Torque resistance describes the ability of a heat set insert to resist rotation when a screw is tightened, loosened, or loaded in service. In a 3D printed part, this resistance comes from the mechanical engagement between the insert knurls and the surrounding plastic, but the printed boss must also be strong enough to transfer rotational load into the larger part structure.
M5 inserts create a different design problem from small inserts. The larger screw can apply much more tightening torque. The insert usually has a larger outside diameter and deeper engagement, but the surrounding printed boss must also be large enough to support that load. If the boss is undersized, the insert may spin, the boss may crack, or the plastic may deform around the insert.
For M5 heat set inserts, torque resistance should be evaluated together with boss outside diameter, wall thickness, edge distance, pilot hole tolerance, installation heat, screw engagement length, and material creep behavior. A larger insert does not automatically create a stronger joint if the printed structure around it is not large enough.
Typical Reference Factors for M5 Torque Resistance
The table below provides typical reference values and engineering starting points. These are not guaranteed torque ratings. Actual torque resistance depends on insert series, knurl pattern, printed material, print orientation, pilot hole fit, boss geometry, insertion temperature, and screw tightening method.
| Design Variable | Effect on M5 Torque Resistance | Risk if Poorly Controlled | Engineering Note |
|---|---|---|---|
| Insert Size | M5 provides larger thread engagement and higher fastening capacity than smaller inserts | Higher screw torque can overload the printed boss if the structure is undersized | M5 should be treated as a structural fastening node, not just a larger thread. |
| Insert Outside Diameter | Larger OD increases knurl contact area and rotational grip | If boss OD does not scale with insert OD, the surrounding plastic may fail first | Boss design should begin from the actual insert OD and knurl geometry. |
| Knurl Engagement | Creates mechanical interlock against insert spin | Weak engagement can cause insert rotation during tightening or removal | Torque resistance depends on plastic flow into the knurls during installation. |
| Pilot Hole Fit | Controls plastic displacement and insert seating pressure | Oversized holes reduce grip; tight holes may crack or distort the boss | M5 pilot holes need controlled tolerance because installation force and heat are larger. |
| Boss Outside Diameter | Provides surrounding plastic volume to resist rotational stress | Small boss OD can lead to spin, cracking, or local wall deformation | For M5, boss OD must be generous enough to transfer torque into the part body. |
| Boss Wall Thickness | Supports the insert against radial and rotational loading | Thin walls may split, bulge, or soften around the insert | M5 bosses require more wall support than smaller insert sizes. |
| Boss Base Thickness | Transfers tightening load into the main printed structure | A weak base may deform or tear even if the insert does not spin | Torque and preload can both damage the boss base if the load path is weak. |
| Screw Tightening Torque | Directly controls rotational load applied to the insert | Over-tightening may spin the insert or crack the boss | Hand tightening can easily exceed what a printed boss can resist if no torque control is used. |
| Material Behavior | Controls stiffness, creep, heat response, and deformation resistance | PLA may crack; PETG may creep; ABS may soften if overheated | Material selection becomes more important as insert size and torque increase. |
Recommended Design Rules
- Design M5 torque resistance from the printed structure, not only the insert. The insert may be strong, but the boss must carry rotational load into the surrounding part.
- Scale boss OD with insert OD. An M5 insert needs a larger boss than smaller insert sizes. Using a compact boss around a large insert often moves failure into the plastic wall.
- Control pilot hole tolerance carefully. An oversized hole can reduce knurl engagement and cause spin. A tight hole can crack or distort the boss during installation.
- Provide enough wall thickness around the insert. M5 tightening torque can create high radial and rotational stress in the boss wall.
- Do not ignore boss base thickness. A strong boss wall is not enough if the base below the insert cannot transfer load into the part.
- Use controlled screw tightening where possible. M5 screws can generate more torque than small printed bosses can tolerate, especially when tightened by hand with large tools.
- Consider heat input during installation. Larger inserts need more heat energy. Too much heat can soften the boss; too little heat can prevent proper knurl engagement.
- Check whether M5 is too large for the available printed geometry. If the part cannot provide enough boss OD, wall thickness, and edge distance, M4 or a different fastening strategy may be more reliable.
Material Adjustments for PLA, PETG, and ABS
PLA
PLA can provide good stiffness and crisp knurl engagement after installation, which may help initial torque resistance. However, PLA is brittle and can crack when the pilot hole is too tight, the boss wall is thin, or the screw is over-tightened.
For M5 torque resistance in PLA, the main risk is sudden boss cracking. Because M5 screws can apply higher torque, PLA bosses should use generous wall thickness, controlled insertion temperature, and conservative tightening practices. A stiff PLA boss may feel strong until it fractures.
PETG
PETG is tougher and more ductile than PLA, which can reduce immediate cracking during M5 insert installation. However, PETG may relax under sustained preload and repeated tightening cycles.
For M5 torque resistance in PETG, the common risk is gradual loss of rotational grip or preload stability. The boss may not crack at first, but plastic around the insert can creep, deform, or loosen over time. PETG M5 bosses need enough wall thickness, stable seating depth, and controlled screw torque.
ABS
ABS can work well for functional printed assemblies, especially where heat and impact resistance matter. However, M5 insert installation requires more heat than smaller inserts, and excessive heat can soften the ABS boss too much.
For M5 torque resistance in ABS, the key is controlled installation heat and pressure. Overheating may smear the plastic around the knurls, reduce mechanical lock, or allow the insert to sink or tilt. Proper cooling and vertical seating are important for stable torque resistance.
Common Torque Failure Modes
Torque resistance should be checked together with M5 heat set insert installation quality.
1. Insert Spin During Tightening
Insert spin occurs when the screw tightening torque exceeds the rotational grip between the insert and the printed boss. This usually happens when the pilot hole is oversized, the knurl engagement is weak, the boss wall is undersized, or the screw is tightened too aggressively.
2. Insert Spin During Screw Removal
Some M5 inserts do not spin during the first tightening but rotate when the screw is removed later. This can happen when screw threads bind, preload is high, the material relaxes around the insert, or the insert was not fully seated during installation.
3. Boss Wall Cracking
M5 torque can crack the boss wall if the boss outside diameter or wall thickness is too small. PLA is especially vulnerable to sudden cracking, but PETG and ABS can also fail if the geometry is too compact or the insert is too close to an edge.
4. Local Plastic Deformation
Local deformation occurs when the plastic around the insert yields, creeps, or softens instead of holding the insert rigidly. This is common when the installation heat is too high, the screw preload is excessive, or the material relaxes over time.
5. Boss Base Failure
In larger insert sizes such as M5, the insert may remain locked in the boss wall while the base below the boss deforms or tears. This means the problem is not only insert grip but the load path from the boss into the larger printed part.
6. Insert Tilt Under Torque
If the insert is installed off-axis or the screw enters at an angle, tightening torque becomes uneven. One side of the insert carries more load than the other, which can reduce torque resistance, damage the boss wall, and increase the chance of spin.
Why M5 Torque Resistance Is Different from M3 and M4
M5 inserts provide more fastening capacity than M3 or M4, but they also demand more from the printed part. The screw is larger, the applied torque is higher, the insert requires more heat to install, and the boss must carry greater rotational and preload forces.
In M3 and M4 designs, the limiting issue is often compact geometry or insufficient wall thickness. In M5 designs, the limiting issue is often whether the printed boss and surrounding part are structurally large enough to justify using an M5 insert at all.
M5 is useful when the part has enough material volume to support it. If the part is thin, narrow, close to an edge, or printed in a material with poor creep resistance, M5 can create a stronger screw connection than the plastic can realistically support.
When M5 Torque Resistance Is Usually Appropriate
- Large printed fixtures with enough boss volume
- Functional brackets with moderate structural loading
- Parts where a larger screw is needed for assembly stiffness
- Thicker printed components with generous edge distance
- Applications where screw tightening can be controlled
When M5 May Be Too Large for the Printed Boss
- The boss wall must be thin because the part envelope is limited.
- The insert is close to an outer edge, slot, corner, or cutout.
- The screw will be tightened with a large tool and no torque control.
- The printed material is prone to creep, softening, or weak layer adhesion.
- The boss base is shallow or poorly connected to the main part body.
- The joint carries vibration, impact, or repeated service loads without enough structural support.
Related Engineering Guides
- M5 Heat Set Insert Dimensions Reference for 3D Printed Parts
- M5 Heat Set Insert Hole Size for 3D Printed Parts
- M5 Heat Set Insert Boss Design for 3D Printed Parts
- M5 Heat Set Insert Pull-Out Strength for 3D Printed Parts
- Torque Resistance of Heat Set Inserts in 3D Printed Parts
- Boss OD Ratio for Heat Set Inserts in 3D Printed Parts
- Heat Set Insert Pilot Hole Tolerance Reference for 3D Printed Parts
- Heat Set Insert Minimum Wall Thickness Reference for 3D Printed Parts
- Screw Engagement Length for Heat Set Inserts in 3D Printed Parts
- PLA vs PETG vs ABS for Threaded Inserts
FAQ
What controls M5 heat set insert torque resistance?
M5 heat set insert torque resistance is controlled by insert outside diameter, knurl engagement, pilot hole fit, boss outside diameter, boss wall thickness, boss base support, material behavior, installation heat, and screw tightening torque.
Why does an M5 heat set insert spin in a 3D printed part?
An M5 insert usually spins when the screw tightening torque exceeds the grip between the insert knurls and the surrounding printed plastic. Oversized pilot holes, weak boss support, poor seating depth, material creep, and over-tightening can all cause insert spin.
Is M5 always stronger than M4 in 3D printed parts?
No. M5 can provide more fastening capacity, but only if the printed boss and surrounding part are large enough to support it. If the boss is undersized, M5 may create more stress than the printed plastic can handle.
Does PETG provide good M5 torque resistance?
PETG can tolerate installation stress better than PLA, but it may relax under sustained preload. PETG M5 bosses need enough wall thickness, stable seating depth, and controlled screw tightening to maintain torque resistance over time.
When should I avoid M5 heat set inserts?
Avoid M5 when the printed part cannot provide enough boss OD, wall thickness, edge distance, or base support. M5 may also be risky in thin covers, narrow brackets, weak materials, or joints tightened without torque control.
Related Decision Resources
For insert selection, tool choice, and supplier comparison, use these decision-focused references after the engineering requirements are defined.