
M5 heat set insert boss design for 3D printed parts requires generous boss diameter, wall thickness, hole depth, edge distance, base support, and controlled installation heat. M5 inserts can provide strong fastening, but they also place high demand on the surrounding printed structure.
An M5 insert is not just a larger version of an M3 insert. It introduces more heat, more plastic displacement, higher screw torque, and greater load transfer into the printed part. For this reason, the boss must be designed as a structural feature rather than a small cylinder around a hole.
This guide explains how to design M5 heat set insert bosses for large 3D printed parts, structural brackets, fixture bodies, mounting blocks, covers, panels, and prototype assemblies.
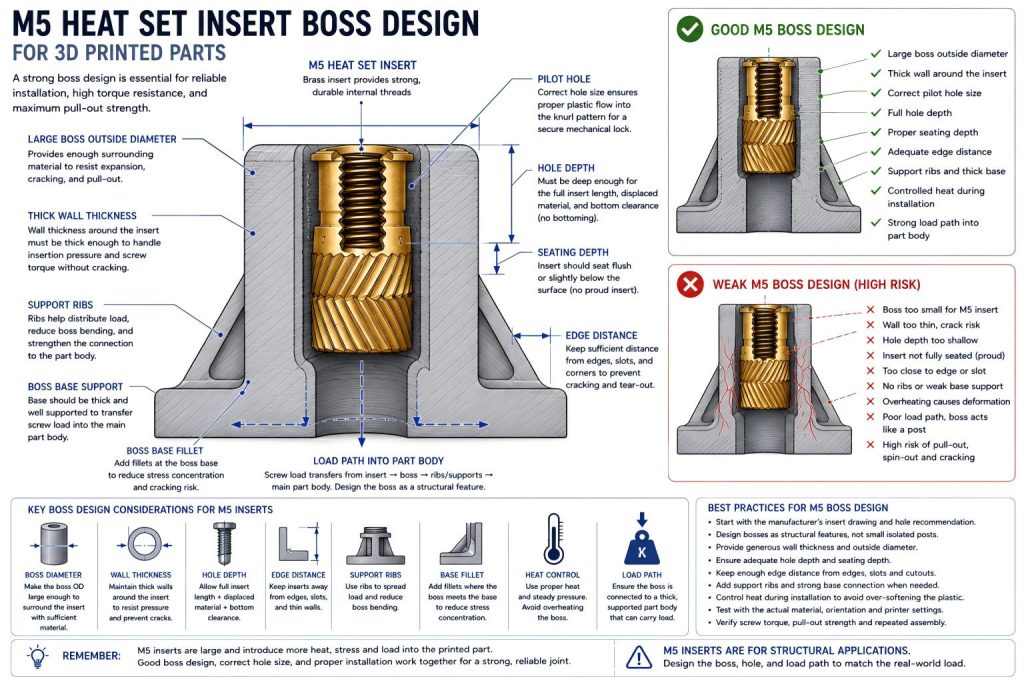
Why M5 Boss Design Matters
M5 heat set inserts are often used when a printed part needs stronger screw fastening than smaller insert sizes can provide. They may be used in fixture plates, machine guards, mounting blocks, large covers, equipment housings, and structural prototypes.
However, a large insert can only create a strong joint if the printed boss can support it. If the boss is too thin, too shallow, too close to an edge, or poorly connected to the part body, the insert may damage the boss during installation or fail under load.
Common M5 boss design problems include:
- Boss cracking during heat insertion
- Insert tilt caused by high insertion force
- Plastic bulging around the seating surface
- Insert spin-out under high screw torque
- Pull-out failure under axial load
- Boss base cracking under bending or prying loads
- Overheating or deformation of the surrounding printed structure
M5 Boss Design Requires More Than Scaling Up M3
Simply scaling up an M3 boss does not automatically create a reliable M5 boss. The larger insert changes the installation and loading conditions.
An M5 insert usually requires:
- More wall thickness around the insert
- More hole depth for full seating
- More boss outside diameter
- Better edge distance
- Stronger support at the boss base
- More control over heat input
- A clearer load path into the main printed part
If the surrounding part cannot provide this support, an M4 insert, through-bolt, captured nut, or redesigned fastening layout may be safer.
Key Boss Design Variables for M5 Heat Set Inserts
| Design Variable | Why It Matters |
|---|---|
| Boss outside diameter | Provides enough surrounding material to resist expansion, cracking, and pull-out. |
| Wall thickness | Thin walls around an M5 insert are a major risk during installation and service. |
| Pilot hole size | Controls plastic displacement, insertion force, and knurl engagement. |
| Hole depth | Must allow full insert seating, displaced plastic, and screw engagement clearance. |
| Edge distance | M5 inserts near edges or slots may crack or tear out under load. |
| Boss base support | The base must transfer screw load into the main printed part. |
| Support ribs | Ribs can help distribute load and reduce boss bending. |
| Print orientation | Layer direction affects cracking, pull-out, and boss base strength. |
| Material | PLA, PETG, ABS, ASA, nylon, and filled materials respond differently to heat and load. |
| Installation heat | M5 inserts store more heat and can over-soften the printed boss. |
Boss Outside Diameter for M5 Inserts
The boss outside diameter must provide enough plastic around the M5 insert to resist installation pressure and service load. A narrow boss around a large insert can crack during insertion or lose strength when screw torque is applied.
For M5 bosses, the outside diameter should be reviewed together with:
- Insert outer knurled diameter
- Wall thickness around the pilot hole
- Expected tightening torque
- Pull-out and prying load
- Material stiffness and ductility
- Distance to nearby edges or corners
- Whether ribs or a support pad connect the boss to the part body
The boss should be large enough to work as a structural load-transfer feature, not just as a thin ring around the insert.
Wall Thickness Around an M5 Insert
Wall thickness is one of the most important M5 boss design variables. M5 inserts displace a larger volume of plastic during installation. If the wall is too thin, the boss may crack, expand, or deform outward.
Thin walls also reduce torque resistance because the surrounding plastic cannot fully support the insert’s knurl engagement zone.
For M5 insert bosses, changing the pilot hole alone is rarely enough if the surrounding wall is weak. The boss geometry itself must be strong.
Hole Depth and Seating Depth
M5 inserts are often longer than smaller inserts, so hole depth and seating depth must be checked carefully.
A boss should provide enough depth for:
- Full insert length
- Target seating position
- Displaced plastic
- Bottom clearance in blind holes
- Screw engagement length
- Stack-up tolerance
If the hole is too shallow, the insert may bottom out, sit proud of the surface, tilt during insertion, or reduce usable screw engagement. If the insert is pushed too deep, the screw stack-up may no longer clamp the assembly correctly.
Edge Distance for M5 Bosses
M5 inserts should not be placed too close to a free edge, thin wall, corner, slot, or cutout. A large insert near an edge can create a crack path during installation or service load.
Low edge distance can lead to:
- Cracks from the insert hole to the outside edge
- Boss splitting during heat insertion
- Reduced pull-out strength
- Lower torque resistance
- Part edge deformation under clamp load
- Failure under vibration or prying load
If the M5 insert must be near an edge, the surrounding structure should be reinforced with a larger local pad, ribs, thicker walls, or a different fastener layout.
Boss Base Support and Load Path
The boss base is critical for M5 insert strength. A large insert can transfer significant screw load into the boss, and that load must continue into the printed part body.
If the boss sits on a thin plate or unsupported wall, the boss may act like a tall post and crack at the base. If the boss is connected to a thick local pad or supported with ribs, the load can spread more effectively.
Good M5 boss base design should consider:
- Base thickness
- Fillets at boss transitions
- Ribs connected to the load direction
- Local pads under the boss
- Whether the boss is loaded in bending or prying
- Whether the load path reaches the main part body
Support Ribs Around M5 Bosses
Support ribs are often useful for M5 bosses because they help distribute load and reduce local bending. They are especially helpful when the boss rises from a flat plate, fixture body, panel, or cover.
Ribs should be thick enough to print reliably and should connect the boss to meaningful surrounding structure. Very thin ribs may look supportive in CAD but add little real strength in a printed part.
For M5 bosses, ribs should support the load path rather than only decorate the boss.
Material Behavior in M5 Boss Design
PLA
PLA can provide stiff structure but can crack when an M5 insert creates high radial pressure. M5 bosses in PLA should have generous wall support, enough edge distance, and controlled insertion heat.
PETG
PETG is more ductile than PLA and may tolerate insertion pressure better, but it can deform under sustained clamp load or heat. M5 PETG bosses should be checked for long-term preload retention and repeated assembly behavior.
ABS and ASA
ABS and ASA may handle heat better, but boss strength still depends on print quality, layer adhesion, and geometry. Warping or weak layer bonding can reduce M5 boss reliability.
Nylon and Filled Materials
Nylon and fiber-filled materials may offer useful toughness, but their behavior depends on formulation, moisture, fiber content, and print settings. M5 bosses in these materials should be validated with real printed samples.
Print Orientation and Layer Direction
M5 insert bosses may carry higher loads, so print orientation should be reviewed carefully. If the load opens weak layer lines, the boss may split or pull away from the part body.
Review whether:
- The insert axis is parallel or perpendicular to layer lines
- The boss base is built from continuous material
- The screw load creates pull-out, bending, or prying stress
- The ribs are aligned with the load path
- The part will experience vibration or repeated assembly
Large insert size cannot compensate for poor layer orientation in a highly loaded part.
Heat Control During M5 Installation
M5 heat set inserts store more heat than smaller inserts. This makes heat control a major part of boss design.
If the boss is overheated, the hole may enlarge, the wall may soften, and the insert may lose mechanical engagement after cooling. If the insert is underheated, installation force may crack the boss.
Good M5 installation requires:
- Controlled heat input
- Vertical alignment
- Steady insertion pressure
- Avoiding excessive dwell time
- Allowing the boss to cool before loading the screw
- Checking that the insert seats flush or slightly below the surface
Designing M5 Bosses for Torque Resistance
M5 screws can apply more tightening torque than smaller screws. The boss must resist the insert rotating inside the plastic during tightening or removal.
Torque resistance depends on:
- Insert knurl design
- Pilot hole fit
- Plastic flow around the insert
- Boss wall thickness
- Material stiffness and creep behavior
- Installation heat
- Final screw torque
- Repeated assembly cycles
If the insert spins, the problem may involve boss geometry, hole fit, overheating, weak knurl engagement, or excessive screw torque.
Designing M5 Bosses for Pull-Out Resistance
Boss geometry should also be checked against M5 pull-out strength requirements.
M5 inserts can provide strong pull-out resistance when the printed boss is large, deep, and well supported. However, the boss must be able to transfer axial load into the part body.
Pull-out resistance depends on:
- Insert length
- Knurl engagement depth
- Hole size
- Boss depth
- Wall thickness
- Boss base support
- Material strength
- Print orientation
- Load direction
A large insert in a weak boss may pull out with a larger damaged area rather than produce a stronger joint.
When M5 May Be Too Large for the Part
M5 is not always the correct choice. If the printed part cannot provide enough boss diameter, wall thickness, hole depth, or load path, a smaller insert or different fastening strategy may be better.
Consider alternatives when:
- The boss would be too close to an edge
- The wall thickness would be too thin
- The part cannot support the screw torque
- The hole depth is not sufficient
- The load is safety-critical or impact-heavy
- The printed material creeps under clamp load
- A through-bolt or metal reinforcement would provide a safer load path
Possible alternatives include M4 inserts, multiple smaller fasteners, captured nuts, through-bolts, metal backing plates, or a redesigned mounting structure.
Common M5 Boss Design Mistakes
- Choosing M5 because it looks stronger without checking boss space.
- Making the boss too small around a large insert.
- Using thin walls around the pilot hole.
- Placing the insert too close to an edge or slot.
- Ignoring the larger heat input during installation.
- Using a blind hole that is too shallow.
- Designing the boss as an isolated tall post.
- Ignoring screw torque and clamp load.
- Testing insert fit but not load behavior.
- Assuming insert size alone determines joint strength.
Recommended M5 Boss Design Process
- Select M5 only when the part has enough space and load requirement for a large insert.
- Check the insert drawing for outer diameter, length, and hole recommendation.
- Design the boss with enough outside diameter, wall thickness, and hole depth.
- Check edge distance, base support, ribs, and load path.
- Review print orientation relative to screw load.
- Print a test boss in the final material and orientation.
- Install the insert with controlled heat and vertical pressure.
- Inspect for cracking, tilt, proud seating, plastic bulging, or overheating.
- Test screw torque, pull-out behavior, and repeated assembly if relevant.
- Use a smaller insert or different fastening method if the boss cannot support M5.
Related Engineering Guides
- M5 Heat Set Insert Hole Size for 3D Printed Parts
- M4 Heat Set Insert Boss Design for 3D Printed Parts
- M3 Heat Set Insert Boss Design for 3D Printed Parts
- How to Design Bosses for Heat Set Inserts
- Heat Set Insert Hole Size Guide
- Torque Resistance of Heat Set Inserts in 3D Printed Parts
- Pull-Out Strength of Heat Set Inserts in 3D Printed Parts
- Heat Set Insert Installation Temperature for 3D Printed Parts
Related Engineering References
- M5 Heat Set Insert Dimensions Reference for 3D Printed Parts
- Boss OD Ratio for Heat Set Inserts in 3D Printed Parts
- Heat Set Insert Minimum Wall Thickness Reference for 3D Printed Parts
- Heat Set Insert Edge Distance Reference for 3D Printed Parts
- Heat Set Insert Seating Depth Reference for 3D Printed Parts
- Heat Set Insert Assembly Stack-Up Reference for 3D Printed Parts
Conclusion
M5 heat set insert boss design must account for large insert size, high heat input, high screw torque, deeper hole requirements, wall thickness, edge distance, and load transfer into the printed part.
An M5 insert can create a strong fastening point only when the boss is large enough, deep enough, and well supported enough to handle the installation and service loads. In large 3D printed parts, the boss is not just a hole feature. It is the structure that makes the insert useful.
Related Decision Resources
For insert selection, tool choice, and supplier comparison, use these decision-focused references after the engineering requirements are defined.