
M4 heat set insert dimensions are important when designing stronger 3D printed parts that need reusable metal threads for structural brackets, fixtures, motor mounts, covers, service panels, and load-bearing assemblies.
M4 inserts are larger than M2, M2.5, and M3 inserts, so they can provide more screw engagement and higher fastening capacity. However, they also require more boss diameter, more wall thickness, more installation control, and more printed material around the insert.
This reference explains the main M4 heat set insert dimensions that matter in 3D printed parts, including insert length, outside diameter, printed hole size, boss diameter, boss depth, wall thickness, screw engagement length, pull-out strength, and torque resistance.
M4 heat set insert dimensions are not universal. Different manufacturers use different body diameters, knurl patterns, pilot diameters, lengths, and recommended hole sizes. Always confirm the actual insert datasheet before finalizing the printed hole.
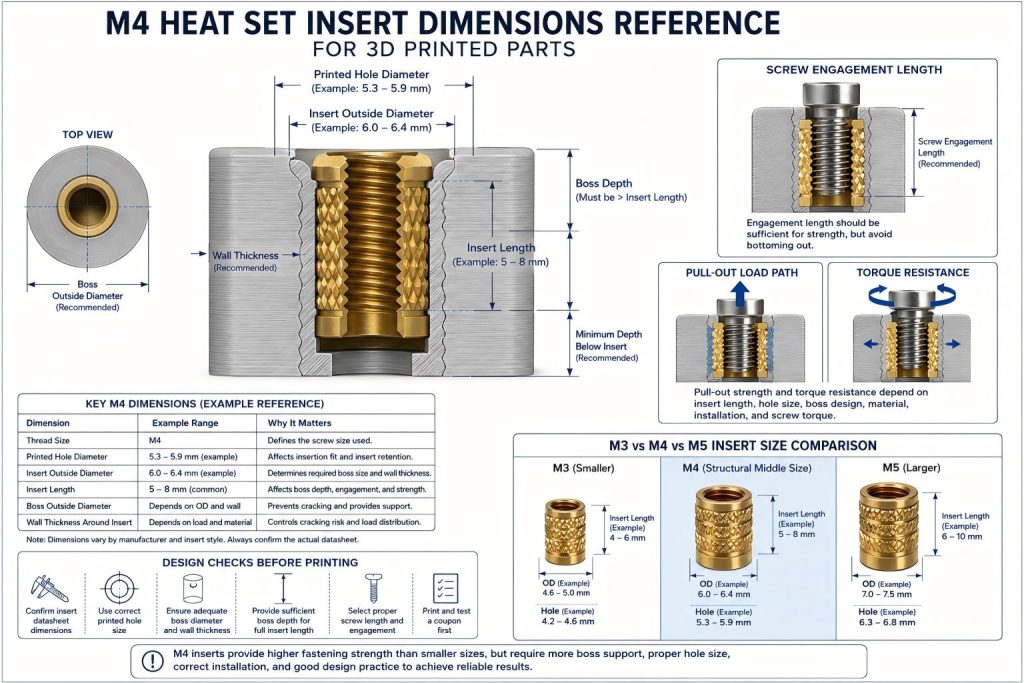
Typical M4 Heat Set Insert Dimensions
A typical M4 heat set insert is a brass threaded insert with an internal M4 thread and an external knurled or patterned body. During heat installation, the surrounding thermoplastic softens and flows around the insert body to create mechanical retention.
As a practical reference, some M4 heat set insert specifications list values around a 5.7 mm printed hole diameter and about 8.3 mm hole depth. Short M4 inserts may use the same hole diameter with a shallower depth. Other M4 insert styles may use different pilot hole sizes, surface hole diameters, outside diameters, and insert lengths.
These values should be treated as example reference dimensions, not universal design rules.
| Dimension | Example Reference Range | Why It Matters |
|---|---|---|
| Thread size | M4 | Defines the screw size used in the assembly. |
| Printed hole diameter | Example: around 5.3–5.9 mm, depending on insert style | Affects insertion fit, plastic flow, boss stress, and insert retention. |
| Insert outside diameter | Example: around 6.0–6.4 mm, depending on insert geometry | Determines how much surrounding boss material is needed. |
| Insert length | Often around 5–8 mm, depending on short or standard style | Affects boss depth, screw engagement, pull-out strength, and seating control. |
| Boss outside diameter | Depends on insert OD, wall thickness, and load requirement | Helps prevent cracking, edge breakout, boss deformation, and weak support. |
| Wall thickness around insert | Depends on load, material, and insert OD | Controls cracking risk, stiffness, and load distribution around the insert. |
For smaller insert comparison, see M2 Heat Set Insert Dimensions Reference for 3D Printed Parts, M2.5 Heat Set Insert Dimensions Reference for 3D Printed Parts, and M3 Heat Set Insert Dimensions Reference.
Why M4 Inserts Need More Boss Support
M4 inserts can provide stronger fastening than smaller insert sizes, but they also remove and displace more plastic during installation. A design that simply scales up from M3 may fail if the boss wall thickness, edge distance, or print orientation is not adjusted.
M4 inserts are commonly used when the assembly needs:
- higher screw clamp force
- stronger reusable threads
- larger covers or panels
- fixture or jig fastening points
- motor mounting brackets
- robot structure connections
- serviceable structural joints
- stronger pull-out resistance than smaller insert sizes
The insert itself may be stronger, but the surrounding printed structure must still be strong enough to support it.
M4 Heat Set Insert Hole Size Considerations
For the next sizing step, see M4 heat set insert hole size.
The printed hole for an M4 heat set insert should be based on the actual insert body geometry, not only on the M4 screw size. M4 refers to the internal thread. The printed hole must match the outside diameter, pilot diameter, knurl geometry, insert length, and supplier-recommended installation dimensions.
A good M4 insert hole should:
- guide the insert straight during installation
- allow enough plastic flow around the knurl pattern
- avoid excessive looseness that reduces torque resistance
- avoid excessive interference that cracks the boss
- provide enough depth for full insert seating
- avoid plastic flow into the internal thread
- avoid overheating and excessive local deformation
Larger inserts such as M4 need more installation control because more heat and displacement are involved. If the hole is too small, the boss may crack or bulge. If the hole is too large, the insert may not develop enough grip.
For broader hole design rules, see the Heat Set Insert Hole Size Guide.
Boss Diameter and Wall Thickness for M4 Inserts
For boss sizing geometry, compare this value with the boss OD ratio reference.
The boss around an M4 heat set insert must provide enough plastic to support the insert during installation, tightening, pull-out loading, and repeated use. Because the insert outside diameter is larger than smaller sizes, the boss must also be larger.
For M4 inserts, boss design should start from the largest outside diameter of the insert, not from the M4 thread diameter. The outer knurled body controls how much material is displaced during installation and how much surrounding plastic is needed for support.
When designing an M4 boss, check:
- largest insert outside diameter
- recommended printed hole diameter
- remaining boss wall thickness
- distance from the insert to nearby edges
- boss depth below the insert
- layer orientation of the printed part
- expected screw tightening torque
- whether the joint is load-bearing or serviceable
For boss geometry principles, see How to Design Bosses for Heat Set Inserts.
Insert Length and Boss Depth
The boss depth should be greater than the insert length. If the boss is too shallow, the insert may bottom out, sit proud of the surface, or push molten plastic into the thread.
M4 inserts are often used in stronger parts, so boss depth should be checked carefully. A shallow boss may appear acceptable in CAD but still fail if there is not enough material below the insert to support axial load.
A practical boss depth check should include:
- the full insert length must fit inside the boss
- there should be enough material below the insert to support the load
- the screw should not bottom out below the insert
- the insert should not be pushed too deep during installation
- the installation tool should not deform surrounding geometry
- displaced plastic should not block the internal thread
If the insert must sit flush with the printed surface, the printed hole depth and installation control become more important.
Screw Engagement Length for M4 Inserts
Screw engagement length should be long enough to provide stable clamping, but not so long that the screw bottoms out inside the insert or below the boss.
M4 screws can apply higher clamp force than smaller screws. This makes screw length selection more important. A screw that is too short may not provide enough thread engagement. A screw that is too long may create false tightening resistance, damage the insert joint, or push against the bottom of the printed cavity.
When selecting screw length, check:
- insert internal thread depth
- part thickness
- mating component thickness
- washer thickness, if used
- required clamp force
- clearance below the insert
- whether the assembly will be opened repeatedly
- whether the joint sees vibration or structural loading
For deeper design logic, see Screw Engagement Length for Heat Set Inserts in 3D Printed Parts.
Pull-Out and Torque Resistance
M4 heat set inserts are often selected when the joint needs stronger pull-out resistance or higher tightening torque than smaller insert sizes can provide. However, the larger insert does not automatically make the printed part strong.
Pull-out strength and torque resistance depend on:
- insert length
- insert outside diameter
- knurl pattern
- printed hole size
- boss diameter
- boss depth
- material behavior
- installation temperature
- screw tightening torque
- load direction
If the boss is too thin, too shallow, or too close to an edge, the printed plastic may fail before the metal insert reaches its potential strength.
For deeper engineering background, see Pull-Out Strength of Heat Set Inserts in 3D Printed Parts and Torque Resistance of Heat Set Inserts in 3D Printed Parts.
Material Behavior: PLA, PETG, ABS, and Nylon
M4 heat set insert performance depends strongly on the printed material.
PLA is stiff and can provide good dimensional control, but it may crack around tight inserts, thin bosses, or high clamp forces. PETG is tougher, but it may creep under sustained screw preload. ABS can tolerate installation heat better than PLA, but still depends on hole fit and boss design. Nylon and carbon fiber nylon may offer better toughness for structural parts, but printed tolerance, moisture behavior, and local stress concentration should still be checked.
Larger inserts such as M4 can generate more local stress during installation and tightening, so material behavior becomes more important than it may appear in the CAD model.
For material comparison, see PLA vs PETG vs ABS for Threaded Inserts.
M4 vs M3 and M5 Inserts
M4 inserts are often selected when M3 is too small for the expected load, but M5 would require too much space or too much surrounding plastic. M4 is a common middle structural size for brackets, fixtures, covers, and serviceable assemblies.
| Insert Size | Typical Use Case | Design Tradeoff |
|---|---|---|
| M3 | General 3D printed assemblies, covers, brackets, electronics housings | Common and compact, but may be limited for stronger structural joints. |
| M4 | Fixtures, motor mounts, structural brackets, larger covers, service panels | Stronger fastening potential, but needs larger boss geometry and more material. |
| M5 | Larger fixtures, heavy brackets, load-bearing structures | Higher load capacity, but requires even more plastic support and spacing. |
For many 3D printed parts, the best insert size is not simply the largest screw that fits. The surrounding plastic structure must be able to support the insert.
Recommended Design Checks Before Printing
Before finalizing an M4 heat set insert design, check these items:
- Confirm the actual manufacturer dimensions of the insert.
- Measure the largest outside diameter of the insert body.
- Confirm the recommended hole size from the supplier.
- Add enough boss wall thickness around the insert.
- Add enough boss depth for the full insert length.
- Confirm screw length and thread engagement.
- Check edge distance and nearby thin walls.
- Check whether the joint will see pull-out, torque, vibration, or repeated assembly.
- Print a test coupon before committing to the final part.
- Test insertion temperature and screw tightening torque after cooling.
For M4 inserts, a test coupon is especially useful because the larger insert can produce more heat, more plastic displacement, and more local boss stress during installation.
Common M4 Heat Set Insert Design Mistakes
Using the M4 Screw Size as the Hole Size
The printed hole should match the insert body geometry, not the screw thread size. M4 refers to the internal thread, not the outside diameter of the insert.
Hole Too Large
If the printed hole is too large, the melted plastic may not fully flow into the knurl pattern. This can reduce torque resistance and allow the insert to spin.
See also: Why Do Heat Set Inserts Spin in 3D Printed Parts?
Hole Too Small
If the hole is too small, the insert may force too much plastic outward during installation. This can crack the boss, deform the wall, or push plastic into the thread.
See also: Why Do Bosses Crack Around Heat Set Inserts?
Boss Too Thin
If the boss is too thin around the insert, the structure may crack during insertion or fail during screw tightening. M4 inserts need enough plastic around the insert body, especially when used in structural brackets or fixtures.
Insert Too Close to an Edge
M4 inserts are often used in larger parts, but they can still fail if placed too close to an edge, slot, or cutout. The larger insert body needs more surrounding material to distribute load.
See also: Why Do Heat Set Inserts Fail Near Edges or Corners?
Screw Too Long
A screw that is too long may bottom out inside the insert or below the insert. This can push the insert upward, damage the boss, or create false tightening torque.
No Test Coupon
Because M4 inserts are larger and often used in stronger assemblies, print tolerance and installation control matter. A test coupon can reveal whether the hole prints too tight, too loose, oval, rough, or inconsistent across materials.
Practical Reference Summary
M4 heat set insert dimensions should be treated as insert-specific engineering data, not as a universal value. The most important dimensions are insert length, outside diameter, knurl diameter, printed hole size, boss wall thickness, boss depth, and screw engagement length.
M4 is useful when M3 is too small and M5 requires too much space. It can be a strong option for structural 3D printed assemblies, but only if the boss geometry, hole size, screw length, material behavior, and load path are checked together.
A good M4 insert design is not just a larger metal thread in a printed hole. It is a load-bearing fastening structure that must survive heat installation, screw tightening, pull-out load, torque, repeated use, and long-term material behavior.
FAQ
What is a typical hole size for an M4 heat set insert?
Some M4 heat set insert references list hole sizes around 5.7 mm, while other insert styles use different pilot or surface hole diameters. The correct hole size depends on the insert manufacturer, geometry, printed material, and printer tolerance.
Can I use the same hole size for all M4 heat set inserts?
No. M4 heat set inserts can have different outside diameters, knurl profiles, pilot shapes, and lengths. The printed hole should match the actual insert geometry and supplier recommendation.
Is M4 stronger than M3?
M4 can provide more screw engagement and larger insert body area than M3, but the actual strength depends on boss design, material behavior, hole size, insert length, and load direction.
When should I use M4 instead of M3?
M4 may be useful when M3 does not provide enough clamp force, pull-out resistance, or screw strength for the application. It is often used in brackets, fixtures, service panels, motor mounts, and stronger printed assemblies.
Why do M4 inserts crack 3D printed bosses?
M4 inserts can crack bosses if the hole is too small, the boss wall is too thin, the insert is overheated, or the surrounding material cannot absorb the displacement during installation.
Should I print a test coupon for M4 heat set inserts?
Yes. M4 inserts are large enough that installation heat, hole tolerance, and boss geometry can strongly affect the result. A test coupon helps verify hole size, insertion depth, installation temperature, and screw tightening behavior before using the design in a final part.
Related Guides
- M3 Heat Set Insert Dimensions Reference
- Heat Set Insert Hole Size Guide
- How to Design Bosses for Heat Set Inserts
- Screw Engagement Length for Heat Set Inserts in 3D Printed Parts
- Pull-Out Strength of Heat Set Inserts in 3D Printed Parts
- Torque Resistance of Heat Set Inserts in 3D Printed Parts
- Why Do Heat Set Inserts Fail Near Edges or Corners?
- PLA vs PETG vs ABS for Threaded Inserts
Source Notes
Example M4 heat set insert dimensions vary by supplier and insert style. Always confirm the specific datasheet for the insert being used before finalizing a production design.
Related Decision Resources
For insert selection, tool choice, and supplier comparison, use these decision-focused references after the engineering requirements are defined.