
Heat Set Inserts for 3D Printed Clamp Blocks are used when a printed clamp, fixture block, holding block, guide block, or workholding component needs reusable metal threads for repeated tightening, adjustment, and clamping force.
A clamp block is different from a simple mounting bracket. The screw is not only holding two parts together. It may create clamp force, resist sliding, press against a workpiece, hold a rail, secure a tube, lock an adjustment, or preload a fixture. This means the insert, boss, screw engagement, material, and load path must be designed for repeated tightening and localized force.
Heat set inserts can improve thread durability in clamp blocks, but they do not automatically make a printed clamp strong. The printed structure must still resist pull-out, insert spin, boss crushing, clamp pad deformation, screw preload loss, and creep under sustained load.
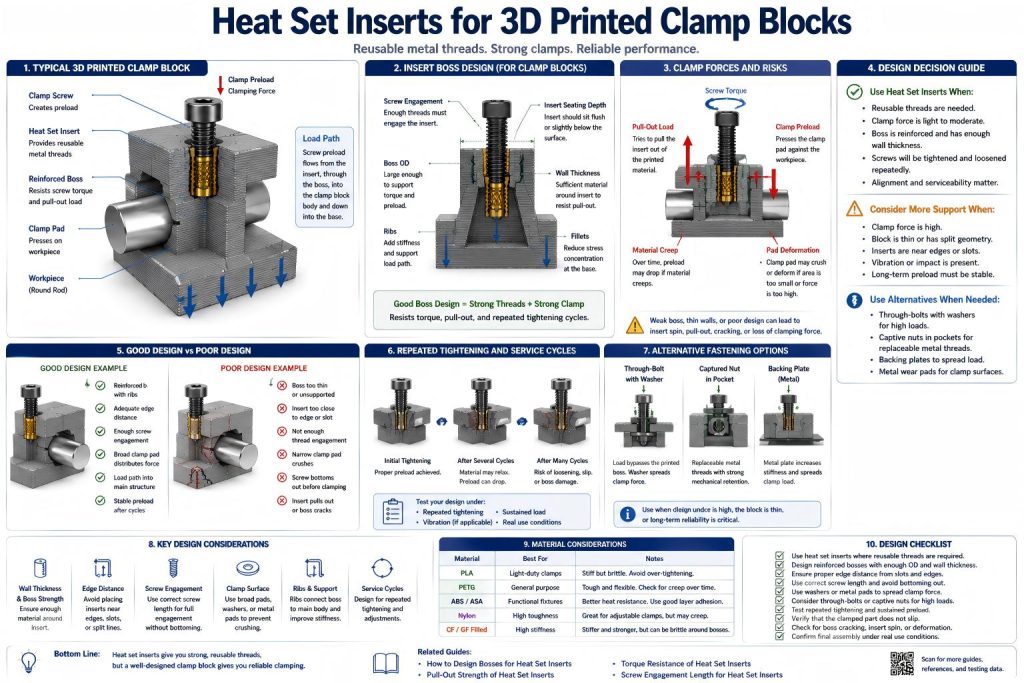
Why Clamp Blocks Need Careful Insert Design
A clamp block creates force by tightening a screw. That force may press a moving part, clamp a tube, lock a fixture, or hold a replaceable component. The screw force usually concentrates around the insert and the clamp contact area.
If the insert boss is weak, the insert may spin or pull out. If the clamp surface is too soft, the part may crush or deform. If the screw bottoms out before clamping, the joint may feel tight but not actually hold. If the printed material creeps, the clamp may loosen after time.
For clamp blocks, the insert must be designed as part of a clamping system, not just as a reusable threaded hole.
Common Use Cases
3D printed clamp blocks appear in fixtures, jigs, machine accessories, guide systems, test setups, workshop tools, robotics, sensor positioning, and prototype workholding.
- tube clamp blocks
- rod and rail clamp blocks
- fixture holding blocks
- sensor clamp brackets
- adjustable stop blocks
- workholding accessories
- printed jig clamps
- alignment blocks
- camera or sensor lock blocks
- prototype machine clamps
- low-load tool holders
- small-batch production fixtures
For related fixture applications, see Heat Set Inserts in 3D Printed Industrial Fixtures, Heat Set Inserts in 3D Printed CNC Fixture Plates, and Heat Set Inserts for Printed Jigs with Replaceable Wear Plates.
How Clamp Loads Affect Heat Set Inserts
Clamp blocks often create repeated screw preload. The screw may be tightened and loosened many times during adjustment, maintenance, or part changeover. This makes thread durability important, which is why heat set inserts are useful.
However, clamp force creates several load paths:
- axial screw preload into the insert
- torque during tightening
- pull-out force if the clamp tries to open
- side load if the clamped part shifts
- compression at the clamp pad
- creep under sustained clamp force
- vibration or movement during use
- repeated service cycles from adjustment
The insert provides the metal thread, but the printed clamp body must carry these loads into the rest of the part.
Insert Location in Clamp Blocks
Insert location should follow the clamp load path. If the screw presses directly into a workpiece, the insert boss must support tightening torque and preload. If the screw holds a clamp cover or split block, the insert location must resist the block opening under load.
Common insert locations include:
- clamp screw bosses
- split block closing screws
- adjustment lock screws
- replaceable clamp pad screws
- fixture plate attachment points
- rail or rod locking screw positions
- service screws for removable clamp components
Good insert placement keeps the screw load aligned with reinforced geometry instead of forcing a small boss to behave like the entire clamp.
Clamp Screw Load Path
The clamp screw should transfer force into a reinforced printed structure. If the insert sits in a narrow thin wall, the clamp force may crack the boss or deform the part before useful clamping is achieved.
A good clamp load path usually includes:
- a reinforced insert boss
- enough material behind the screw load
- ribs or thick geometry around the clamp area
- a broad clamp surface or pad
- a direct load path into the main block body
- avoidance of sharp internal corners
- controlled screw length and engagement
- enough edge distance from slots and split lines
For load-bearing insert decisions, see Should I Use Heat Set Inserts in Load-Bearing 3D Printed Parts?.
Boss Design for Clamp Blocks
The boss around a clamp insert must resist installation heat, screw tightening torque, pull-out force, and repeated preload. A weak boss may install cleanly but fail after repeated clamp cycles.
A clamp block boss should provide:
- enough boss outside diameter
- enough wall thickness around the insert
- enough depth for insert seating
- proper screw engagement length
- fillets at boss transitions
- ribs connecting the boss to the clamp body
- edge distance from split lines, slots, and clamp openings
- print orientation that resists splitting under clamp force
For boss geometry, see How to Design Bosses for Heat Set Inserts, Boss OD Ratio for Heat Set Inserts in 3D Printed Parts, and Heat Set Insert Minimum Wall Thickness Reference for 3D Printed Parts.
Screw Engagement and Clamp Force
Clamp blocks often need more reliable screw engagement than simple covers. If the screw is too short, the clamp may strip or loosen. If the screw is too long, it may bottom out before the clamp force is applied.
This is especially important when the clamp block includes washers, clamp plates, replaceable pads, or split-block geometry.
Check the final stack-up:
- screw head
- washer if used
- moving clamp plate or cover
- printed clamp body
- insert seating depth
- available thread engagement
- bottom clearance
- actual clamp contact surface
For screw engagement behavior, see Screw Engagement Length for Heat Set Inserts in 3D Printed Parts. For stack-up planning, see Heat Set Insert Assembly Stack-Up Reference for 3D Printed Parts.
Clamp Pad Deformation and Boss Crushing
A clamp block can fail without the insert pulling out. The clamp contact area may deform, crush, creep, or lose shape under sustained screw force. If the clamp pad deforms, the screw preload drops and the clamped object may slip.
Clamp pad deformation is common when:
- the contact area is too small
- the material is soft or creep-prone
- the clamp force is too high
- the screw presses through a narrow point
- there is no washer or pressure-spreading surface
- the part is loaded for a long time
- the clamp sees vibration or thermal cycling
Useful design improvements include wider clamp pads, replaceable pads, washers, metal contact plates, thicker clamp surfaces, or geometry that mechanically locates the clamped part instead of relying only on friction.
Repeated Tightening and Service Cycles
Clamp blocks are often adjusted repeatedly. This makes heat set inserts useful because the screw engages metal threads instead of wearing plastic threads. But repeated tightening still affects the printed boss and clamp surface.
Repeated clamp cycles can cause:
- insert spin during tightening
- boss cracking near the insert
- screw preload variation
- thread wear if the insert is damaged
- clamp surface indentation
- material creep under clamp force
- part slipping after several cycles
- loss of alignment after reassembly
For repeated service decisions, see Should I Use Heat Set Inserts for Parts That Need Frequent Disassembly?.
When Through-Bolts May Be Better
Some clamp blocks should use through-bolts instead of heat set inserts. A through-bolt can spread clamp load through the full part thickness and use washers, nuts, or backing plates to reduce local boss stress.
Consider through-bolts when:
- clamp force is high
- the clamp block is thin
- the insert would be close to a split line or edge
- the boss cannot be reinforced enough
- the clamp sees vibration or repeated load
- failure would damage the assembly
- the clamp needs a washer or backing plate to spread load
- the screw should clamp across the full block thickness
For through-bolt decisions, see Should I Use Through-Bolts Instead of Heat Set Inserts in 3D Printed Parts?.
Heat Set Inserts vs Captive Nuts in Clamp Blocks
Captive nuts can be useful in clamp blocks when the load is higher or when the printed material should not carry the full thread load around an insert. A captive nut pocket can provide a replaceable metal thread while allowing the printed geometry to hold the nut mechanically.
| Thread Method | Best Use | Main Concern |
|---|---|---|
| Heat set insert | Reusable internal threads in supported bosses | Boss must resist torque, pull-out, and repeated preload. |
| Through-bolt with nut | Higher clamp load and full-thickness load transfer | Needs rear access, nut space, and washer support. |
| Captive nut | Replaceable metal thread in printed pocket | Pocket must resist nut rotation and breakout. |
| Embedded metal plate | High load or repeated clamp force | More complex assembly but spreads load better. |
The best clamp design often separates functions: geometry locates the part, screw preload clamps it, and metal hardware provides durable threads.
Material Considerations
Material choice strongly affects clamp block performance. A material that works for a light bracket may deform under sustained clamp force.
| Material | Clamp Block Behavior | Insert Design Note |
|---|---|---|
| PLA | Stiff, but brittle and sensitive to heat or shock | Use low to moderate clamp force and generous fillets. |
| PETG | Tough, but may creep under sustained clamp load | Check preload loss and slipping over time. |
| ABS / ASA | Useful for functional clamp blocks with better heat tolerance | Check layer adhesion and boss support. |
| Nylon | Tough and flexible, but may creep under clamp pressure | Use locating geometry and avoid relying only on friction. |
| Fiber-filled materials | Stiff and dimensionally stable, but stress concentrations matter | Use fillets, ribs, and tested insert holes. |
For material comparison, see PLA vs PETG vs ABS for Threaded Inserts and Layer Adhesion and Heat Set Insert Strength in 3D Printed Parts.
Print Orientation and Clamp Strength
Clamp blocks can split along layer lines if the load pulls across weak print orientation. This is especially important near split clamp openings, screw bosses, and narrow bridge sections.
Print orientation affects:
- boss splitting
- insert pull-out
- clamp arm flex
- crack growth near screw holes
- slip resistance under load
- long-term clamp stability
For clamp blocks, print orientation should be selected around the expected clamp force and screw direction, not only print convenience or surface quality.
Common Failure Modes
Clamp blocks usually fail because the printed structure cannot maintain force over repeated tightening or sustained load. The insert may be part of the problem, but the clamp body often sets the real limit.
- insert spin during tightening
- insert pull-out under clamp load
- boss cracking near the screw
- clamp pad crushing
- material creep and preload loss
- clamped object slipping
- split block cracking at the slot
- screw bottoming out before clamping
- layer separation around the boss
- washer or screw head crushing printed plastic
For related failure explanations, see Why Do Heat Set Inserts Spin in 3D Printed Parts?, Why Do Heat Set Inserts Pull Out of 3D Printed Parts?, and Why Does Screw Preload Drop in 3D Printed Insert Joints?.
Testing Clamp Blocks
Clamp blocks should be tested under the real use condition. A clamp may feel strong during first tightening but loosen after time, vibration, or repeated adjustment.
A useful test should include:
- final printed material
- final insert type and size
- final screw length and washer stack-up
- intended clamp force
- repeated tightening cycles
- sustained load or creep test
- vibration or movement if relevant
- inspection for insert spin or boss cracking
- checking whether the clamped object slips
- checking whether preload drops after time
Design Checklist
- Use heat set inserts when clamp screws need reusable metal threads.
- Reinforce insert bosses with enough wall thickness, ribs, and fillets.
- Keep inserts away from split lines, edges, slots, and thin tabs.
- Check screw length to prevent bottoming before clamping.
- Use washers, metal pads, or backing plates when clamp force is high.
- Use through-bolts or captive nuts when the printed boss cannot carry the clamp load.
- Use locating geometry so the clamp does not rely only on friction.
- Choose material and print orientation for clamp force direction.
- Test repeated tightening, sustained preload, and slipping.
- Do not assume a metal insert makes the whole clamp structural.
Related Engineering Guides
- How to Choose Heat Set Inserts for 3D Printed Parts
- Pull-Out Strength of Heat Set Inserts in 3D Printed Parts
- Torque Resistance of Heat Set Inserts in 3D Printed Parts
- Screw Engagement Length for Heat Set Inserts in 3D Printed Parts
- How to Design Bosses for Heat Set Inserts
- Layer Adhesion and Heat Set Insert Strength in 3D Printed Parts
Related Selection Questions
- Should I Use Heat Set Inserts in Load-Bearing 3D Printed Parts?
- Should I Use Through-Bolts Instead of Heat Set Inserts in 3D Printed Parts?
- Should I Use Heat Set Inserts for Parts That Need Frequent Disassembly?
Related Applications
For stop features that are adjusted repeatedly, see adjustable stop blocks.
- Heat Set Inserts in 3D Printed Industrial Fixtures
- Heat Set Inserts in 3D Printed CNC Fixture Plates
- Heat Set Inserts for Printed Jigs with Replaceable Wear Plates
- Heat Set Inserts for High-Vibration Motor Mounting Brackets
FAQ
Are heat set inserts useful in 3D printed clamp blocks?
Yes. They are useful when clamp screws need reusable metal threads and repeated tightening. The printed clamp body still needs enough boss support, wall thickness, screw engagement, and load path strength.
Can heat set inserts handle clamp force?
They can handle clamp force when the boss and printed structure are designed properly. High clamp loads may require through-bolts, washers, captive nuts, metal pads, or backing plates.
Why do clamp block inserts pull out?
They may pull out because the boss is too small, the hole is wrong, the screw load is too high, the material creeps, the insert is near a split line, or the clamp force is not transferred into a strong load path.
Should clamp blocks use through-bolts instead?
Through-bolts may be better for high clamp force, vibration, thin clamp bodies, or structural workholding. Heat set inserts are better for supported bosses where reusable internal threads are needed.
What is the biggest design mistake in printed clamp blocks?
The biggest mistake is relying only on the insert to create a strong clamp. The clamp body, pad surface, boss geometry, material, print orientation, and screw stack-up all determine the real reliability.