
M5 Brass Heat Set Inserts for 3D Printed Parts are large threaded metal inserts used when printed parts need stronger reusable threads for heavy brackets, large fixtures, structural mounting points, machine accessories, and high-load serviceable assemblies.
M5 inserts can provide more screw engagement, higher preload capacity, and better fastening margin than smaller M3 or M4 inserts. However, M5 is not automatically stronger in a 3D printed part. If the printed geometry cannot support the required boss size, wall thickness, edge distance, seating depth, installation heat, and screw torque, the larger insert may crack the boss, deform the part, or fail through the surrounding plastic.
This page explains where M5 brass heat set inserts make sense, where they create risk, and how to design printed parts around their larger size and higher load potential.
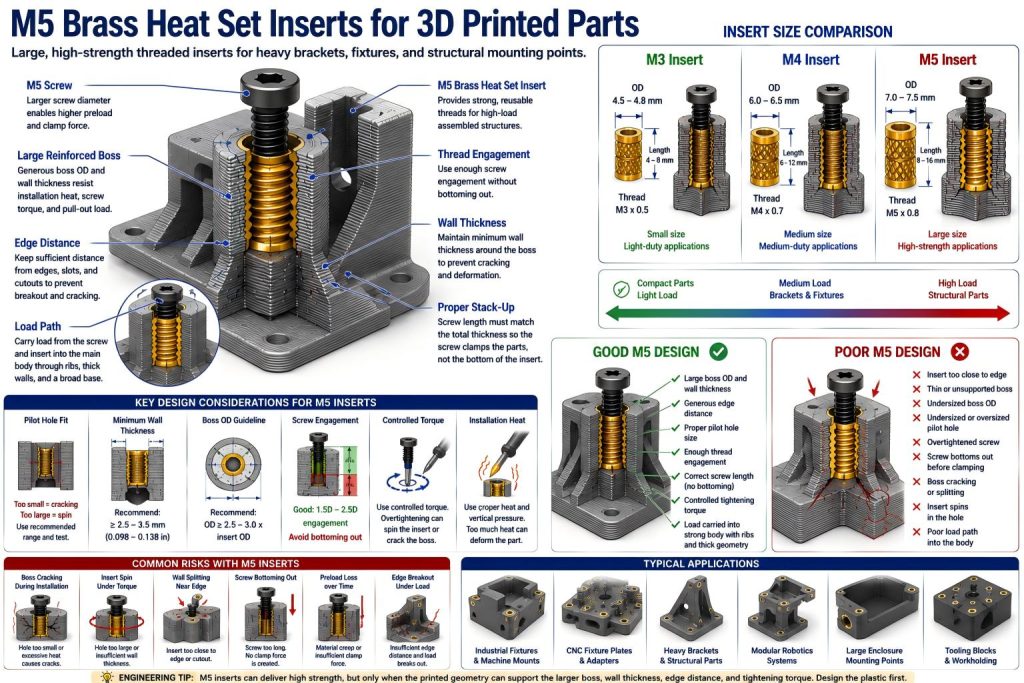
What Makes M5 Brass Heat Set Inserts Different?
M5 inserts are larger than the common M2, M3, and M4 insert sizes used in compact 3D printed assemblies. Their main advantage is fastening capacity. They allow the use of larger screws, deeper thread engagement, higher clamp force, and more durable serviceable joints.
The trade-off is that M5 inserts need significantly more printed material around them. The boss must be larger, the wall must be thicker, the insert must sit far enough from edges and cutouts, and the screw load must transfer into a strong printed structure.
An M5 insert should be treated as part of a load-bearing fastening system, not just a bigger threaded hole.
Common Use Cases
M5 brass heat set inserts are usually used in larger 3D printed parts where the joint needs higher mechanical margin and the part has enough volume to support a large boss.
- large fixture plates
- heavy printed brackets
- machine mounting blocks
- industrial fixture components
- robot base or frame attachments
- structural service panels
- modular tooling blocks
- large workholding accessories
- CNC fixture adapters
- high-load hinge or clamp points
- large battery or electronics enclosure mounts
- printed parts that need stronger repeated assembly threads
For related applications, see Heat Set Inserts in 3D Printed Industrial Fixtures, Heat Set Inserts in 3D Printed CNC Fixture Plates, and Heat Set Inserts in Modular Robotics Systems.
When M5 Inserts Are a Good Choice
M5 inserts are a good choice when the printed part has enough space for a large reinforced boss and the joint needs more strength, preload, or service durability than M4 can reasonably provide.
M5 inserts are often appropriate when:
- the printed part is large enough to support a wide boss
- the joint carries meaningful mechanical load
- the assembly needs higher clamp force
- the part will be serviced or reassembled many times
- the insert is used in a fixture, frame, machine accessory, or structural bracket
- the load path is supported by thick printed geometry
- the insert can be placed far enough from edges and cutouts
- the material and print orientation can support higher screw preload
For repeated assembly behavior, see Heat Set Inserts for Repeated Assembly in 3D Printed Parts.
When M5 Inserts May Be Too Large
M5 inserts become risky when the printed part does not have enough material volume. A large insert placed in a small boss can create more stress than a smaller insert. In that situation, M5 does not strengthen the part. It simply asks weak plastic to carry a larger load.
M5 inserts may be a poor choice when:
- the boss outside diameter is too small
- the printed wall is too thin
- the insert sits near an edge, corner, slot, or cutout
- the part cannot provide enough seating depth
- the screw head or washer area is too large for the assembly
- the load path does not connect into the main printed body
- the material is brittle or has weak layer adhesion
- the joint only needs light-duty fastening
- a well-supported M4 insert would be safer
The best insert size is not the largest size. It is the largest size that the printed geometry can support safely.
M5 vs M4 vs M3 Heat Set Inserts
M5 is often selected for large fixtures and heavy brackets, but it should not be chosen only because it looks stronger. M4 may be the better choice when the part cannot provide enough boss volume for M5. M3 may still be better for compact brackets, electronics covers, and small service panels.
| Feature | M3 Insert | M4 Insert | M5 Insert |
|---|---|---|---|
| Typical use | General brackets, covers, electronics, small assemblies | Fixtures, motor brackets, mechanical panels, medium-load joints | Large fixtures, heavy brackets, structural mounting points |
| Space requirement | Moderate | Higher | Highest |
| Boss size requirement | Moderate | Larger boss needed | Very large boss needed |
| Preload capacity | Moderate | Higher | Highest if geometry supports it |
| Installation risk | Usually manageable | Higher heat and boss stress | Highest heat input and boss stress |
| Best design use | General-purpose fastening | Medium-duty mechanical fastening | Large load-bearing printed structures |
For M4 dimensional planning, see M4 Heat Set Insert Dimensions Reference for 3D Printed Parts. For M5 dimensional planning, see M5 Heat Set Insert Dimensions Reference for 3D Printed Parts.
Boss Design for M5 Inserts
The boss around an M5 insert must be designed as a structural feature. A small boss that might work with M3 or M4 may not safely support the heat, radial expansion, screw preload, and torque associated with M5 hardware.
The most common mistake is enlarging the hole and insert size without enlarging the supporting boss. This can cause cracking during installation, insert spin during tightening, wall splitting, or edge breakout under load.
Important boss design practices include:
- use a large enough boss outside diameter around the insert
- maintain generous wall thickness between the insert and boss edge
- keep M5 inserts far from edges, corners, slots, and cutouts
- connect the boss to the main body with ribs or thick geometry
- avoid tall unsupported boss towers
- use large fillets at boss-to-body transitions
- provide enough insert depth and screw engagement
- avoid placing M5 inserts in thin tabs or narrow flanges
- align the boss with the real load path
- check print orientation so the boss does not split along layer lines
For boss design, see How to Design Bosses for Heat Set Inserts, Boss OD Ratio for Heat Set Inserts in 3D Printed Parts, and Heat Set Insert Minimum Wall Thickness Reference for 3D Printed Parts.
Edge Distance and Load Path
M5 inserts need more edge distance than smaller inserts because the larger screw and insert can apply higher force to the printed material. If the insert is close to an edge, the load may break out through the shortest wall rather than transfer into the part body.
For heavy brackets and fixture blocks, the load path matters as much as the insert itself. The screw force should move from the insert into a thick body, ribbed region, or structural wall. It should not terminate in a thin printed ear or unsupported corner.
Good design usually means:
- placing M5 inserts well inside the part boundary
- avoiding edge-adjacent bosses for high-load joints
- using ribs behind the insert boss
- using broad base geometry under the boss
- aligning the screw load with the strongest printed direction
- avoiding sharp transitions from boss to thin wall
- using washers or broad clamping surfaces where needed
For edge planning, see Heat Set Insert Edge Distance Reference for 3D Printed Parts.
Pilot Hole Size and Installation Sensitivity
M5 inserts displace more plastic during installation than smaller inserts. If the pilot hole is too small, the insert can create high radial stress and crack the boss. If the pilot hole is too large, the insert may not develop enough grip and can spin under screw torque.
Because M5 inserts are often used in functional assemblies, the screw may be tightened more strongly. This makes pilot hole fit, material behavior, and boss support especially important.
Good practice includes:
- measuring the actual insert outer diameter
- printing test coupons for the chosen material and insert style
- checking slicer hole compensation
- allowing for material shrinkage or expansion
- installing the insert square to the boss axis
- using controlled heat and steady pressure
- letting the plastic cool before applying screw preload
- testing insert spin resistance before final assembly
For general hole sizing, see Heat Set Insert Hole Size Guide and Heat Set Insert Pilot Hole Tolerance Reference for 3D Printed Parts.
Installation Temperature and Seating Depth
M5 inserts need more heat than smaller inserts because they have more metal mass and more surface area. The larger heat input can soften a wider area of the printed part. If the boss is too thin or close to a wall, the installation process can distort the geometry before the screw is ever installed.
Seating depth is also important. If the insert sits too proud, the mating component may not sit flat. If the insert is pushed too deep, the boss may deform, the screw stack-up may change, or the insert may interfere with internal geometry.
Important installation points include:
- use controlled heat rather than excessive temperature
- apply steady vertical pressure
- keep the insert square during installation
- avoid forcing the insert before the plastic softens
- avoid pushing the insert below the intended seating depth
- allow the boss to cool before tightening the screw
- check that the mating part sits flat after installation
- check that the screw does not bottom out before clamping
For installation guidance, see Heat Set Insert Installation Temperature for 3D Printed Parts and Heat Set Insert Seating Depth Reference for 3D Printed Parts.
Screw Engagement and Torque Control
M5 screws can create significant clamp force. This is helpful in fixtures and structural mounting points, but it can also damage printed parts if the torque is not controlled.
The screw should engage enough thread to carry the intended load, but it should not bottom out before clamping the assembly. A screw that feels tight may only be hitting the bottom of the insert or hole, leaving the joint with little real preload.
Good practice includes:
- checking screw length against the final assembly stack-up
- using enough thread engagement for the intended load
- avoiding screw bottoming before clamp force is created
- using washers or broad clamp surfaces when needed
- using controlled torque for load-bearing joints
- avoiding hand-tightening by feel in critical assemblies
- checking preload retention after service cycles
- checking for creep in PETG, nylon, and other materials under sustained load
For thread engagement, see Screw Engagement Length for Heat Set Inserts in 3D Printed Parts. For tightening behavior, see Heat Set Insert Torque Range Reference for 3D Printed Parts. For stack-up planning, see Heat Set Insert Assembly Stack-Up Reference for 3D Printed Parts.
Pull-Out Strength and Torque Resistance
M5 inserts can provide high pull-out and torque resistance when the printed structure supports them. The larger insert can grip more plastic and use a larger screw, but the surrounding printed material still controls the real failure limit.
If the boss is too thin, the boss may split. If the insert is too close to an edge, the plastic may break out. If the print has poor layer adhesion, the boss may separate along layer lines. If the screw is overtightened, the insert can spin or crush the surrounding plastic.
Strength should be understood as a system:
- insert diameter
- insert length
- boss outside diameter
- wall thickness
- edge distance
- print orientation
- layer adhesion
- material creep
- screw engagement
- tightening torque
- load direction
- assembly stack-up
For strength behavior, see Pull-Out Strength of Heat Set Inserts in 3D Printed Parts and Torque Resistance of Heat Set Inserts in 3D Printed Parts.
Material Considerations
Material choice strongly affects M5 insert performance because the larger screw can apply higher preload and the installation process adds more heat to the printed boss.
| Material | M5 Insert Behavior | Design Note |
|---|---|---|
| PLA | Stiff, but can crack around large bosses and high preload | Use generous wall thickness, avoid overtightening, and avoid hot environments. |
| PETG | Tougher than PLA, but may relax under sustained M5 preload | Check clamp force loss, creep, and bracket shift after service cycles. |
| ABS | Useful for functional mechanical parts with better heat tolerance | Check layer adhesion, boss support, and installation temperature control. |
| ASA | Useful for exposed brackets and machine-adjacent parts | Maintain edge distance and avoid sharp stress paths near bosses. |
| Nylon | Tough and vibration-tolerant, but may creep under high preload | Use locating geometry and avoid relying only on screw friction. |
| Fiber-filled materials | Stiff and dimensionally stable, but can be less forgiving around stress concentrations | Use fillets, ribs, enough wall thickness, and careful pilot hole testing. |
For material comparison, see PLA vs PETG vs ABS for Threaded Inserts and Layer Adhesion and Heat Set Insert Strength in 3D Printed Parts.
Common Failure Modes
M5 insert failures often happen because the insert size exceeds what the printed geometry can support. The brass insert may be strong, but the plastic around it becomes the soft borderland where failures begin.
- boss cracking during installation
- insert spin under tightening torque
- wall splitting near the boss
- edge breakout under load
- screw bottoming out before clamp force is created
- boss deformation from excessive installation heat
- preload loss in PETG or nylon
- layer separation around the insert boss
- fixture or bracket shifting after repeated service
- overconfidence in M5 size without enough printed support
- load path failure through thin surrounding geometry
For related failure explanations, see Why Do Heat Set Inserts Spin in 3D Printed Parts?, Why Do Bosses Crack Around Heat Set Inserts?, and Why Do Heat Set Inserts Fail Near Edges or Corners?.
Design Checklist
- Use M5 inserts only when the printed part has enough volume for a large supported boss.
- Choose M4 instead when M5 would force thin walls, weak edges, or cramped boss geometry.
- Give the M5 insert generous boss outside diameter and wall thickness.
- Keep M5 inserts away from edges, slots, corners, and cutouts.
- Use ribs or thick geometry to connect the boss to the main part body.
- Align the insert with the real load path.
- Test pilot holes before printing final parts.
- Install with controlled heat and straight vertical pressure.
- Check seating depth so the mating part can sit flat.
- Use correct screw length to avoid bottoming out.
- Use controlled torque for functional or load-bearing joints.
- Test the joint under real load, vibration, and service conditions.
Related Engineering Guides
- How to Choose Heat Set Inserts for 3D Printed Parts
- Heat Set Insert Hole Size Guide
- How to Design Bosses for Heat Set Inserts
- Pull-Out Strength of Heat Set Inserts in 3D Printed Parts
- Torque Resistance of Heat Set Inserts in 3D Printed Parts
- Screw Engagement Length for Heat Set Inserts in 3D Printed Parts
- PLA vs PETG vs ABS for Threaded Inserts
- Layer Adhesion and Heat Set Insert Strength in 3D Printed Parts
Related Insert Type References
- M3 Brass Heat Set Inserts for 3D Printed Parts
- M4 Brass Heat Set Inserts for 3D Printed Parts
- Short vs Long Heat Set Inserts for 3D Printed Parts
- Flanged vs Non-Flanged Heat Set Inserts for 3D Printed Parts
Related References
- M5 Heat Set Insert Dimensions Reference for 3D Printed Parts
- M4 Heat Set Insert Dimensions Reference for 3D Printed Parts
- Heat Set Insert Pilot Hole Tolerance Reference for 3D Printed Parts
- Heat Set Insert Minimum Wall Thickness Reference for 3D Printed Parts
- Heat Set Insert Edge Distance Reference for 3D Printed Parts
- Heat Set Insert Seating Depth Reference for 3D Printed Parts
- Heat Set Insert Assembly Stack-Up Reference for 3D Printed Parts
Related Applications
- Heat Set Inserts in 3D Printed Industrial Fixtures
- Heat Set Inserts in 3D Printed CNC Fixture Plates
- Heat Set Inserts for High-Vibration Motor Mounting Brackets
- Heat Set Inserts in Modular Robotics Systems
- Heat Set Inserts in 3D Printed Small Batch Manufacturing Parts
FAQ
Are M5 brass heat set inserts stronger than M4 inserts?
They can provide more fastening margin than M4 inserts when the printed boss is large enough. If the boss is too small, too thin, or too close to an edge, an M5 insert may damage the printed part instead of making it stronger.
When should I choose M5 instead of M4 inserts?
Choose M5 when the printed part has enough material for a large reinforced boss and the joint needs higher preload, stronger screw engagement, or more structural mounting capacity than M4 can provide.
When should I avoid M5 heat set inserts?
Avoid M5 inserts in thin walls, narrow tabs, compact brackets, weak edges, or parts without enough boss volume. A well-supported M4 insert is often better than an unsupported M5 insert.
Can M5 inserts be used in 3D printed fixtures?
Yes. M5 inserts can be useful in large fixture plates, tooling blocks, clamps, and machine accessories, but the printed structure must support the boss size, screw preload, torque, and load path.
Do M5 inserts require more installation heat?
Usually yes. M5 inserts are larger and require more heat input than smaller inserts. Too much heat can deform the boss, so controlled temperature, correct pilot hole size, and careful seating depth are important.